
The GEA Advantage
As the demand for large-volume products increases, so does the requirement for higher capacity reactors (up to 20,000 L) to realize economies of scale. GEA has responded to the changing needs of biopharmaceutical manufacturers and developed improved technology solutions to optimize both upstream and, with increasing titers, downstream processing, in terms of time and cost efficiency.
Based on its history of innovation and process development, GEA has a thorough working knowledge of therapeutic protein production and has used this competence to design better media and feeding strategies, optimize the fermentation stage and enhance physicochemical conditions during the manufacturing process.
A leading international supplier of integrated process systems, our extensive portfolio of products, technologies and services includes standard and customized fermenters, separators and entire production lines, as well as plant for the production, storage and distribution of clean utilities. Systems for the preparation of media, fluid management, cell cultivation and purification are also part of our global scope of supply.
As a competent manufacturer of complete plant for the life science industries, GEA is a full-service provider of solutions that meet your exact requirements and specifications. From planning, development and installation to qualification and maintenance, our experienced engineers will collaborate with your project team to supply innovative and efficient process solutions for your applications.
Products & Technologies
Showing 4 of 13

Aseptic valves & components
Aseptic valves face exceptionally high demands within UltraClean and Aseptic processes. You can be assured that they all provide highest quality in terms of hygienic design and sustainability.

Centrifugal Separator
GEA separators are designed for liquid-based applications. Using centrifugal force, they are used for separating suspensions consisting of two or more phases of different densities, i.e. they can be used for liquid-liquid separation, for liquid-liquid-solid separation or for liquid-solid separation. They are equally as effective at separating liq...

CIP/SIP Solutions
Innovative CIP concepts of GEA meet comprehensive high standards. Our experts guarantee product safety at every point of the process. Every upgrade is adapted to individual local conditions and customer requirements and leads to noticeable savings.

Homogenizer Compression Block
GEA compression heads are the homogenizer pulsing core since they activate the homogenization process pumping the product at high pressure until it flows inside the homogenizing valve.
Downloads
GEA Insights
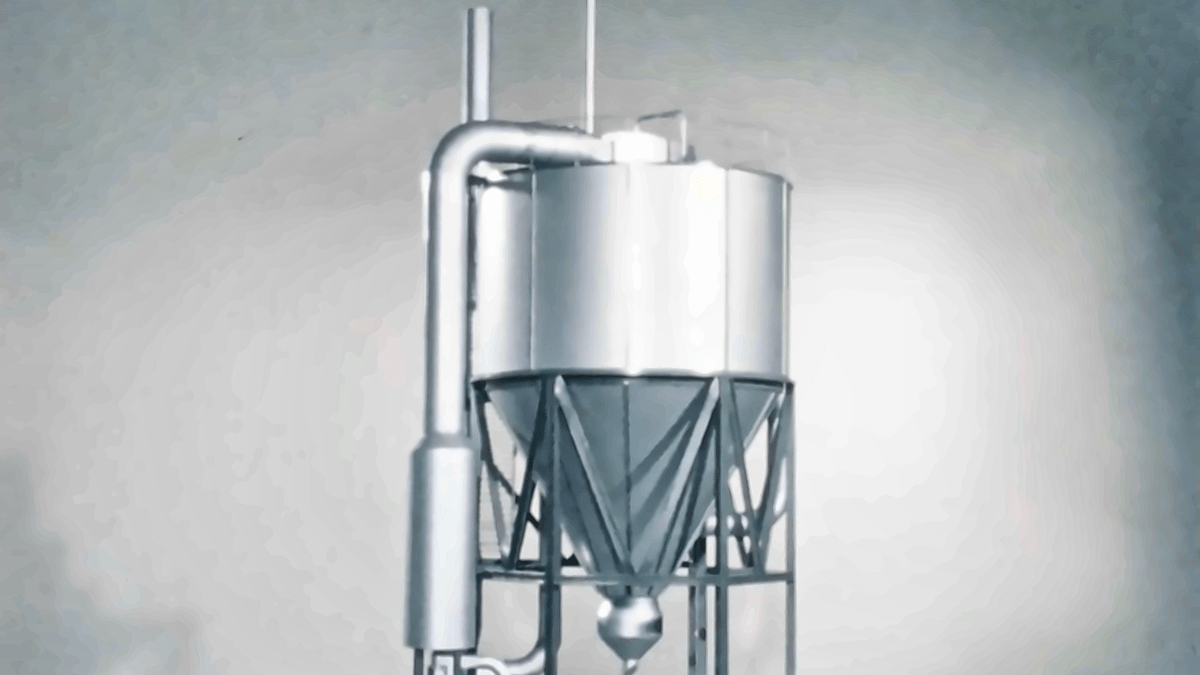
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.

The water equation
Across Europe, drought is a recurring reality – and no longer confined to the south. While water increasingly shapes where industries locate, its value is determined by local context. There are many technological routes to water efficiency in industrial processes, but location, energy needs and other factors are also key.
