


Increase your DCO recovery rates: 3-phase decanters from GEA with Varipond C
Why Choose a 3‑Phase Decanter for DCO Recovery?
1. High Corn Oil Yield from Whole Stillage
3‑phase decanters separate solids, water, and oil in a single, continuous step, making it ideal for recovering corn oil before the actual stillage decanter, or after the evaporation stage.

3-phase decanters separate the whole stillage into DCO, thin stillage and wet distillers grain in one single step.
2. Stable Performance — Even with Process Variability
Stillage composition can vary with upstream fermentation conditions, grind quality, or enzyme performance. A 3‑phase decanter is engineered to handle these fluctuations, maintaining stable dryness, oil separation efficiency, and centrate clarity. The result: consistent DCO recovery, day after day.
3. Lower Energy Consumption in Downstream Processes
By removing more free and emulsified oil early, the remaining thin stillage requires less energy in evaporation and produces a more stable syrup (CDDGS/DDGS). Improved phase separation also reduces load on downstream disk stack centrifuges - cutting energy use and extending equipment life.
4. Maximum Flexibility for Bioethanol Plant Operations
3‑phase decanters integrate seamlessly into both new and existing bioethanol plants. They can be configured to recover oil from whole stillage, thin stillage or syrup and work as the primary or secondary oil recovery step. This flexibility makes it easy to tailor the system to plant capacity, oil yield targets, and process layout.
5. High-Quality Corn Oil Output
With precise control of differential speed, pond depth, and feed conditioning, a 3‑phase decanter produces a clean oil phase with lower moisture and solids. Higher oil purity means better market value and improved downstream handling.
Speaking of control
GEA Varipond C
With GEA Varipond C adjusting your 3-phase decanters to changing feed conditions, flow rates or even feedstocks can be done instantly and directly at the running machine. Just select the respective diameter and the position of the centripetal pump adjusts the separation zone inside the bowl.
It is easy, fast, precise and even easily repeatable if saved as recipe in your control system.
Key benefits for 3-phase DCO and stillage decanters
- Higher DCO recovery from stillage
- Reduced energy costs in evaporation
- Improved DDGS quality thanks to less residual oil
- Stable performance under variable plant conditions
- Robust, low-maintenance design for 24/7 operation
- Optimized integration with existing plant equipment
Boost Revenue and Efficiency with a 3‑Phase Decanter
Whether your goal is to increase corn oil yield, reduce operational costs, or optimize the entire coproduct stream, a 3‑phase decanter delivers measurable advantages across the bioethanol process. By adding this technology, plants can extract more value, improve sustainability metrics, and strengthen overall profitability

GEA Insights
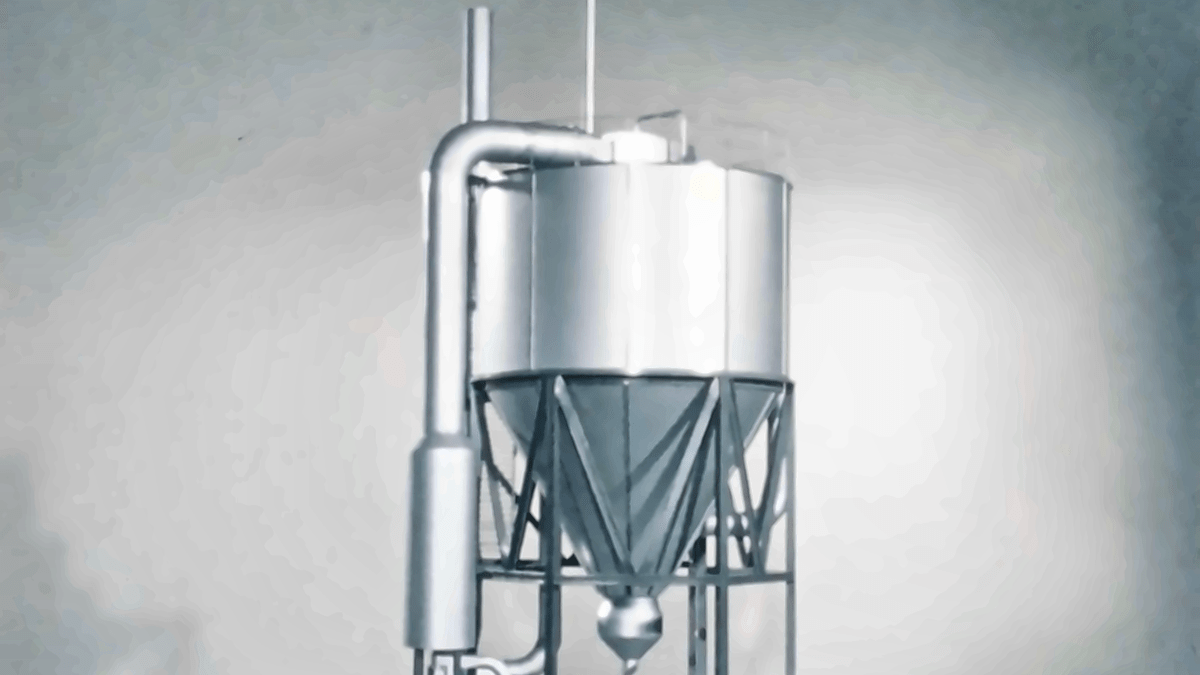
La percée qui a révolutionné le séchage par atomisation
En 1976, les ingénieurs de NIRO répondaient à un défi concurrentiel en repensant ce que pouvait faire le séchage par atomisation. Leur idée est à l'origine du sécheur-atomiseur à plusieurs étages MSD. Cinquante ans plus tard, ce même principe fondamental aide à transformer les liquides en poudres, qui sont utilisées dans des produits nutritionnels essentiels et des médicaments importants partout dans le monde. Perfectionné au cours de plusieurs décennies d'expertise technique, d'enquêtes clientèle et de développement continu, le MSD est une histoire d'innovation aux retombées durables.

Au-delà des machines : exploiter les gisements de performance des installations
Ce n'est pas parce que vous avez des machines efficaces que votre usine l'est. Une trajectoire d'amélioration efficace commence souvent par une analyse qui ne se limite pas aux équipements pris individuellement, et cherche à comprendre comment les processus, les systèmes énergétiques et les décisions opérationnelles s'influencent mutuellement. C'est une démarche holistique, conçue pour repérer des opportunités qui, sans cela, risqueraient de passer inaperçues.

Comment une vanne révolutionne la production des aliments et des boissons
Dans les installations agroalimentaires, les vannes sont généralement actionnées en utilisant de l'air comprimé. La technologie d'actionnement GEA Hydract® Actuation Technology, quant à elle, actionne les vannes en utilisant de l'eau, au sein d'un circuit fermé à commande numérique. Résultat, une vanne peut être maintenue en place de manière exacte et réglée par petits paliers. Cela se traduit par une consommation d'énergie en baisse et un meilleur contrôle.
