


Brine cages in cheese brine pool
Securing first-class cheese brine
Dumping of cheese brine is normally very costly, and in some countries it is even prohibited due to the high salt content of the brine. Purification and recycling of the brine is therefore preferable and can provide advantages such as reduced operating costs and improved cheese quality.
Cheese brine, if not treated properly, can contain large amounts of undesired microorganisms, such as gas-producing lactobacilli, pigment-producing micrococcus, pathogenic bacteria, yeast and mold, which all affect the final cheese quality.
Unlike traditional brine treatment methods such as heat treatment, kieselguhr filtration or the addition of preservatives, microfiltration physically removes the undesired microorganisms, dead cells and physical contaminants from the brine without causing any significant change to its chemical composition.
GEA COLDSAN® has the following key advantages:
- Minimum loss of water and salt
- Clean and clear brine
- Total removal of physical impurities
- Over 99% reduction in total bacteria count
- No undesired enzymatic activity
- No pasteurization involved, therefore no protein denaturation, no precipitation of calcium phosphate, and no changes in pH
- Simple and flexible process and easy operation
- Standardized 'Plug & Play' unit
Larger brine pool volumes and fully automated units can be engineered individually to meet the required specifications.
The COLDSAN® unit can either extract a stream from the brine pool, cool it and send it back to the pool via a microfiltration unit. Therefore, the impurities are constantly removed resulting in higher purity of the brine pool. Alternatively, the feed can be returned to a separate pool exclusively for the clarified brine.
| COLDSAN® 15 | COLDSAN® 30 | COLDSAN® 45 | COLDSAN® 60 | COLDSAN® 75 | COLDSAN® 90 | COLDSAN® 120 | |
| Number of modules | 1 | 2 | 3 | 4 | 5 | 6 | 8 |
| Module size | 6" | 6" | 6" | 6" | 6" | 6" | 6” |
| Area m2 | 28 | 56 | 84 | 112 | 140 | 168 | 224 |
| Flow l/day | 15.000 | 30.000 | 45.000 | 60.000 | 75.000 | 90.000 | 120.000 |
| Flow l/h | 750 | 1.500 | 2.200 | 3.000 | 3.800 | 4.500 | 6.000 |
NOTE: The data above are theoretical figures only cannot be guaranteed. The calculated flows are based on clean cheese brine.
Downloads
Related Products

Custom-Designed Filtration Plants
GEA custom designs membrane filtration systems that best utilize the technologies of microfiltration, ultrafiltration, nanofiltration, or reverse osmosis for each customer's specific application.

Condensate Polisher
Condensate from evaporation plants is used as boiler feed water, process, cooling, and rinsing water or is directly discharged into a drainage ditch. For this purpose, the condensate must be purified. Impurities in the condensate can be removed by membrane filtration, in the particular case by reverse osmosis, and high condensate qualities can be...

CIP Recovery Unit
It is now possible to recover more than 90 percent of a spent caustic solution by using pH-resistant nanofiltration (NF) membranes. Benefits include reduced operating costs and better performance.

GEA MICRO FORMULA® for microparticulation
The GEA MICRO FORMULA® uses a special combination of standard flow components and plate heat exchangers to generate microparticulated whey protein concentrates (WPC) with precisely defined particle sizes and functional characteristics. These microparticulated WPC can be used to replace fat or milk protein in many dairy and food applications.

GEA Insights
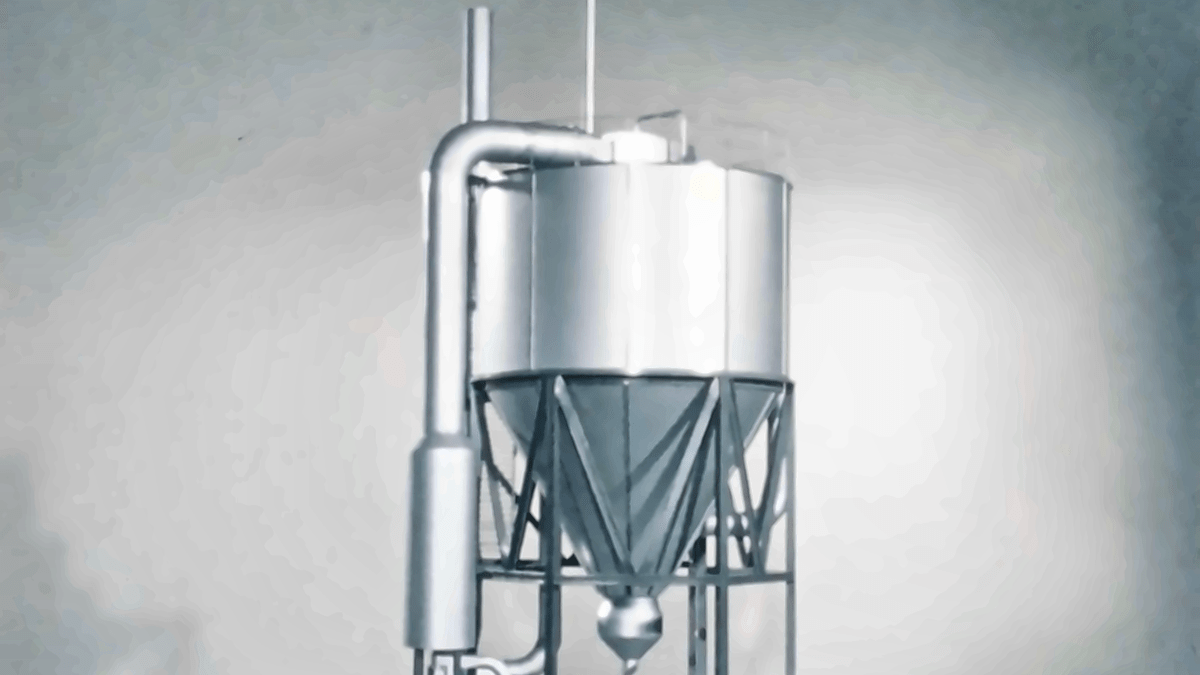
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.

Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.

How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
