
Producing Microbial Food Cultures
Microbial food cultures (MFCs) are live bacteria, yeasts and moulds used in the manufacture of a wide range of human and animal foods: from fermented vegetable products such as sauerkraut and soy sauce, to cheese and yogurts. While starter cultures are MFC preparations which enhance the flavor, taste, color, texture and nutritional value, probiotic cultures are living microorganisms which can benefit health. But keeping billions of microbes alive and viable demands great care.
Starter Culture
Manufacturers often want to produce individual microbial strains. Yet there are hundreds of types of probiotic and starter cultures in production, and it is important that the equipment that manufacturers use helps to avoid cross-contamination. The starting point in the production is generally a ‘mother culture’ supplied, highly concentrated, in deep-frozen form.
Fermentation
Fermentation Fermentation In the laboratory, this concentrate is used to make a pre-culture solution, which is in turn grown – and scaled-up – via a cultivation fermenter and a pre-fermenter to a full-scale fermentation stage operating at a capacity of several thousand litres.
Separation
After cultivation in the fermenters, the biomass has to be gently separated, under aseptic conditions, from the fermentation solution in which it has multiplied. This stage requires great care as the microbes are effective only if they remain alive. Shear stresses at the separation stage can be damaging. The concentrated cells can then be processed by freeze or spray drying and subsequent pelletizing.
Freeze drying
The most common next step for starter cultures is freeze drying. Once frozen, the cultures can survive over long shelf lives. This enables individual cultures to be blended, at a later date, in accordance with specific starter culture recipes before final packaging.
Spray Drying
In the case of probiotic products, manufacturers generally opt for spray dryers with fluid bed drying as the next stage. The lower the water content of the bacteria, the higher their survival rate.
Pelletizing
In dairy applications, concentrated cultures can be fed directly from the separator into liquid nitrogen so that they are immediately deep frozen. They can then be processed into small pellets which are packaged and stored in deep frozen form.
Products & Technologies
Showing 4 of 13

Aseptic valves & components
Aseptic valves face exceptionally high demands within UltraClean and Aseptic processes. You can be assured that they all provide highest quality in terms of hygienic design and sustainability.

Centrifugal Separator
GEA separators are designed for liquid-based applications. Using centrifugal force, they are used for separating suspensions consisting of two or more phases of different densities, i.e. they can be used for liquid-liquid separation, for liquid-liquid-solid separation or for liquid-solid separation. They are equally as effective at separating liq...

Homogenizer Compression Block
GEA compression heads are the homogenizer pulsing core since they activate the homogenization process pumping the product at high pressure until it flows inside the homogenizing valve.

Homogenizing Valves
Homogenizing valve is one of the most important elements of GEA homogenizers to make happen the homogenization products effectively.
Downloads
GEA Insights
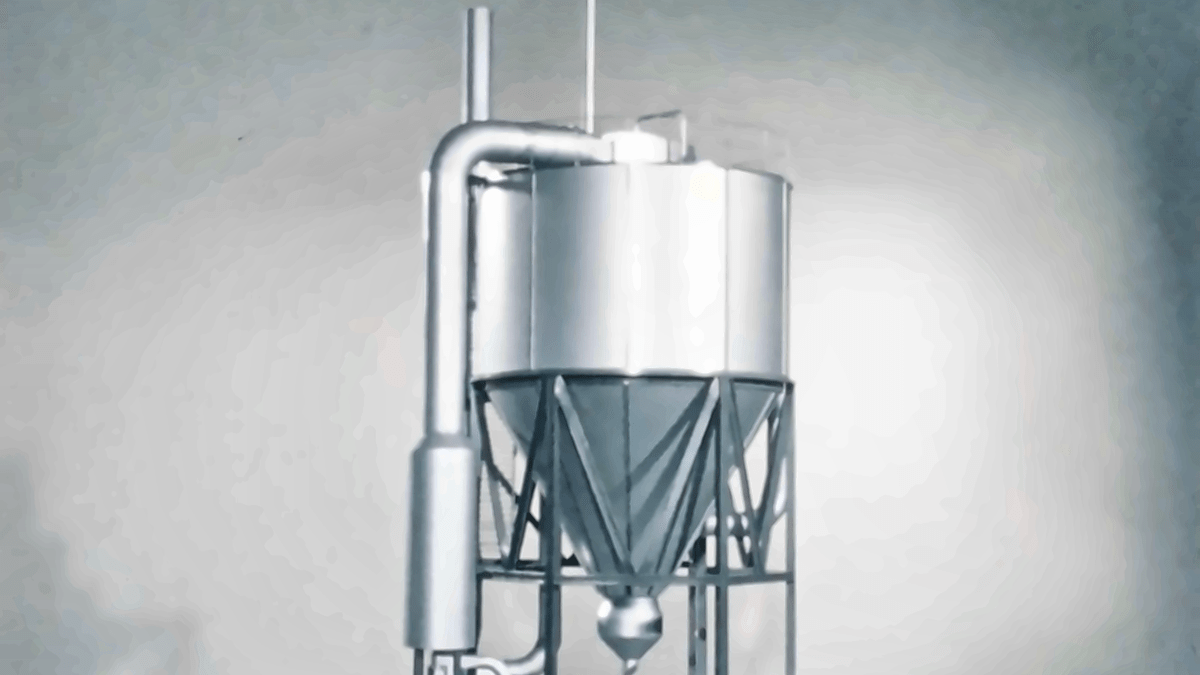
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.
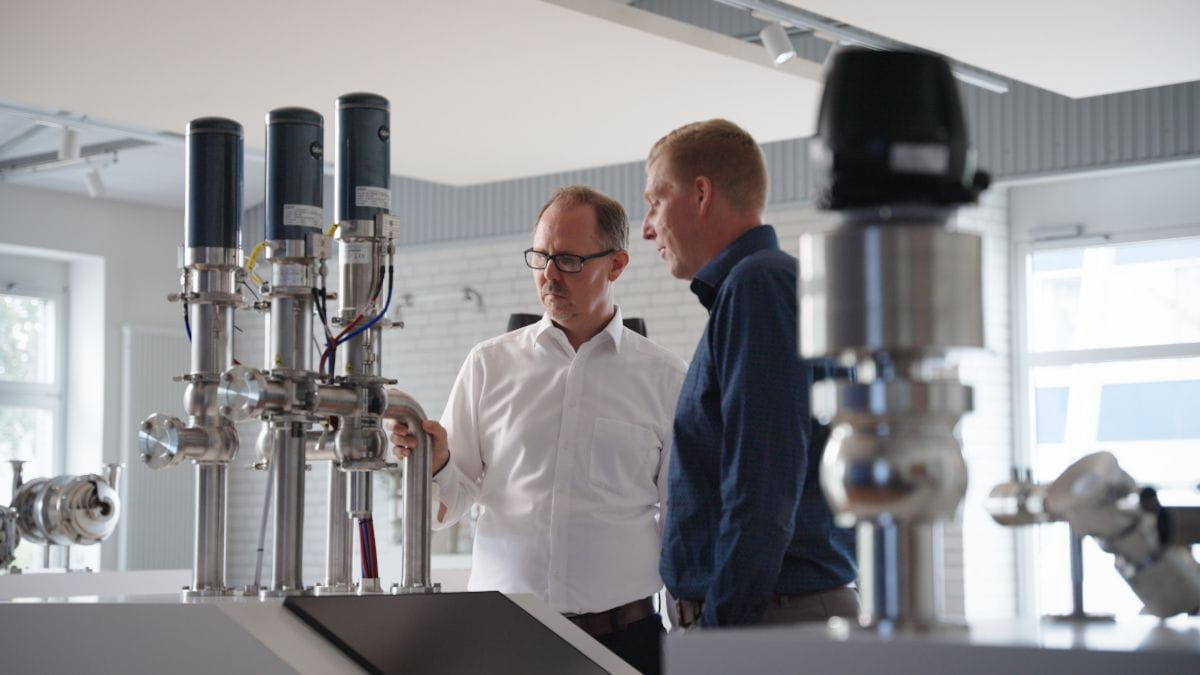
How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
