
Integrated powder handling solutions
The best results from a powder handling system are achieved when each step fits seamlessly into the complete process. GEA combines process and industry expertise with system integration capabilities to develop complete solutions, from spray drying and freeze drying through powder handling to packing. Trust in one experienced partner for the complete process and you benefit from technologies designed to work together, backed by expertise at dedicated testing facilities providing data to support system design, and a global service network and lifecycle support.
 Product quality & yield
Every step in a powder handling process can affect the value and quality of your product. GEA systems are designed to help minimize dust and product loss while protecting product integrity throughout the handling process. Our systems can help you achieve more consistent quality and better value from your products and process.
 Hygiene & cleanability
Hygienic powder handling starts with equipment that’s designed with cleaning in mind. GEA systems can help to reduce contamination risks and simplify cleaning, supporting high hygiene standards, while making day-to-day operation and product changeovers easier.
 Reliability & uptime
Reliable powder handling is an essential part of an efficient production process. GEA solutions are designed to support consistent, dependable operation, helping to reduce disruptions and unplanned downtime, and keeping your process running smoothly.
Industries we serve
Discover GEA Powder Handling products and solutions.
Products and solutions
Pneumatic Conveying

Powder storage and buffering
Conveying, feeding and dosing
Screening and grading
Powder sampling

Loading / Unloading systems

Contained Materials Handling Systems
Automation and system integration
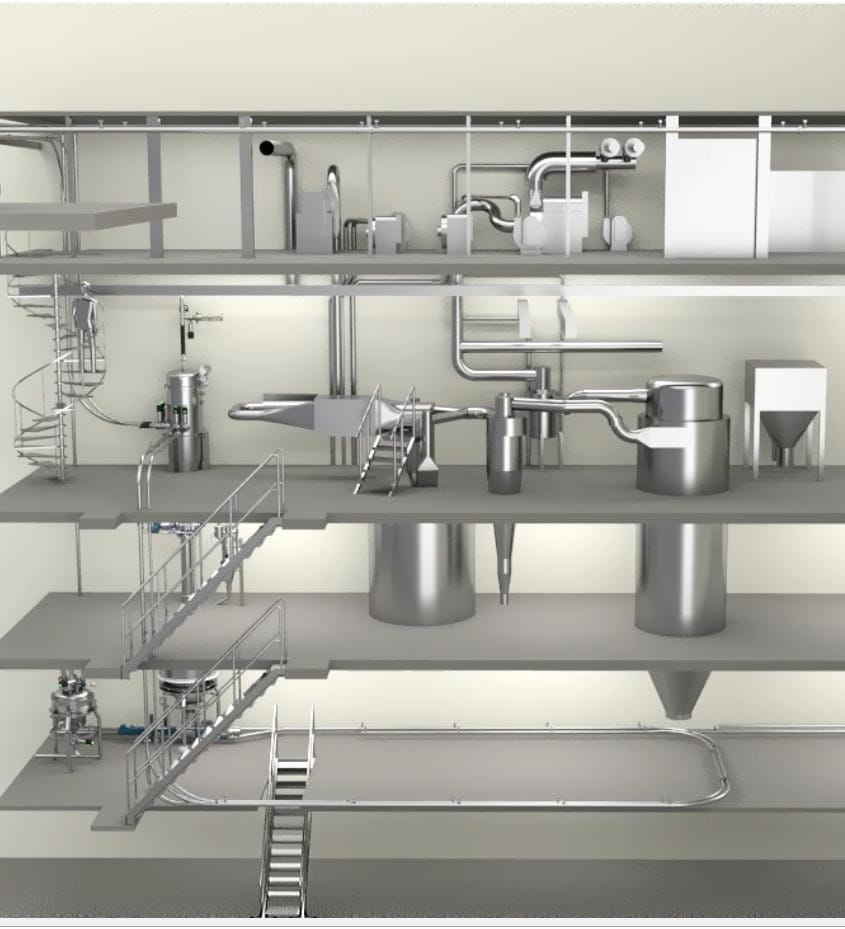
GEA brings individual technologies together into one integrated process that can span spray drying and freeze drying, through to powder handling, storage and buffering, and packing. Buffer storage helps decouple continuous drying from packing campaigns, providing flexibility for product release, cleaning and operational interruptions. Integrated automation supports the complete process with functions such as route selection, inventory monitoring, weighing, recipe control and reporting. By considering the process as a whole we can design stages that work effectively together and provide one point of responsibility for the integrated solution.
See system integration in action
Explore the GEA Process Line Tour to see how individual technologies and process steps can come together as part of a complete production line. Zoom in on Powder handling & storage to explore the technologies and solutions that connect the different stages of the process.

Trials at GEA powder handling test center
Understanding how a powder behaves is key to designing the right handling system. At our test center we can analyze powder properties such as compressibility, moisture content, flowability and fluidization behavior. These insights help us configure powder handling and transport solutions tailored to dairy, food ingredients, chemicals and coffee powders.

Service and lifecycle support
Common questions about powder handling
Yes. GEA develops integrated solutions that combine conveying, storage, feeding and packing technologies with process engineering and automation. The scope is defined around your product and production requirements, with technologies designed to interface with upstream and downstream equipment.
Selecting the best system will depend on powder properties, required throughput, conveying distance, plant layout and hygiene requirements. GEA considers all relevant factors when selecting an appropriate conveying method. Product trials can provide data to support system design and configuration.
Conveying velocity, transfer points and discharge conditions can all affect powder quality. Tests with your product can help to evaluate how proposed handling conditions will affect key powder properties. The results then support the selection and configuration of conveying and feeding technologies to help limit particle breakdown and fines generation.
Buffer storage allows drying and packing to operate on different schedules. A dryer can continue producing while packing takes place in planned campaigns, subject to available storage and product release requirements. This strategy also provides flexibility for cleaning and operational interruptions.
Equipment design and cleaning systems are selected and configured according to product and hygiene level requirements. Configuring systems with access for inspection, suitable contact surfaces and discharge helps to support effective cleaning. When considering system design as a whole it’s also important to think about requirements at product changeover.
Yes. At GEA’s Powder Handling Pilot Plant in Søborg, Denmark, we can evaluate pneumatic conveying using dense and lean phase transport under pressure or vacuum. Trials with your product provide data to support technology selection and system dimensioning.
Depending on the agreed project scope, automation can include conveying routes, destination confirmation, silo inventory, feeding, weighing and packing sequences. Recipe control, alarms and batch reporting can reduce reliance on routine manual actions and support traceability.
Yes. Future capacity, additional products and packing formats can be considered during initial design. Allowances may include space for additional storage, extra conveying destinations and controls expansion. The available capacity must be assessed for each proposed extension.
The best safety strategy will depend on the powder’s dust characteristics, operating conditions and applicable local requirements, and should be considered at the start of system design. Product-specific data will inform the safety assessment process and so selection and configuration of protection measures, where required.
Useful inputs include powder properties, required throughput, operating hours, storage needs and packing formats. Your plant layout, conveying distances, available height, cleaning requirements and future expansion plans will also help us to define a suitable solution.
Products
Showing 4 of 13

25kg Bag tipping stations
The 25kg bag tipping stations are designed to efficiently and hygienically discharge 25kg bags of powder.

ALUS® Load & Unload of Lyophilizers
ALUS® Automatic Load & Unload Systems minimize the risk of operator/product contamination while loading and unloading a freeze dryer.

FIBC emptying stations
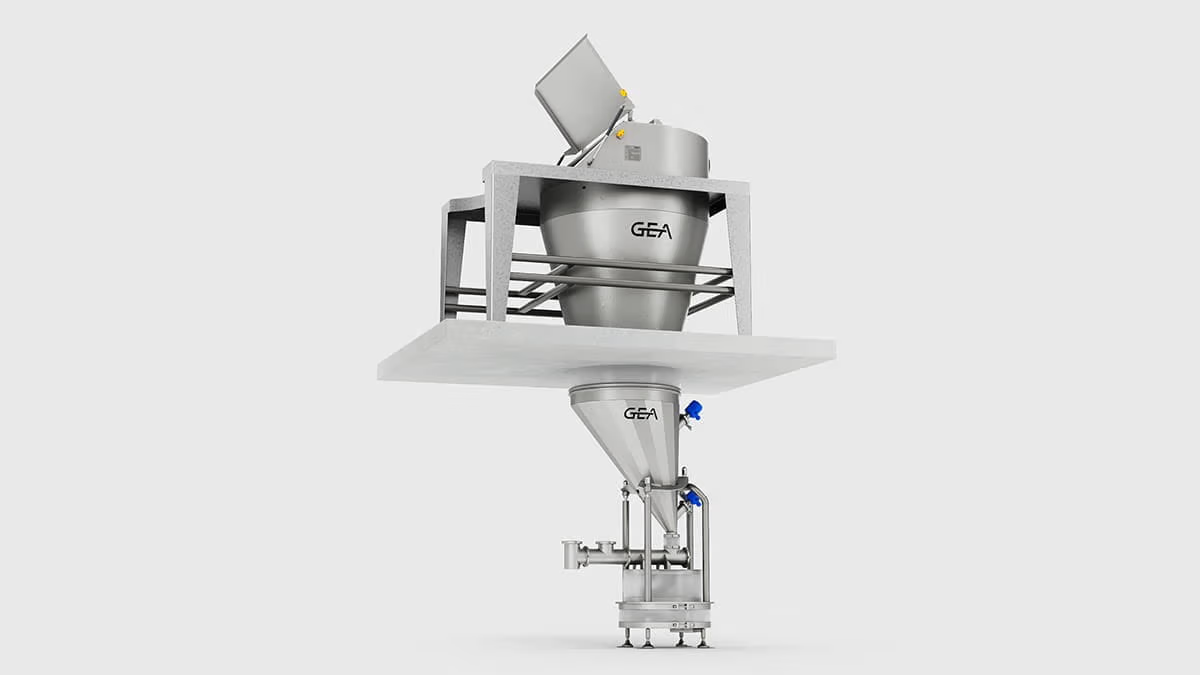
The GEA FIBC emptying stations is designed to enable a single operator to discharge bulk bags of product into a powder process system.

GEA Powder Sampler (PAS)
GEA powder samplers have been designed to complement the powder filling systems we supply. Our auger sampler can take representative powder samples at the point where the powder enters the bag even when packing in inert atmosphere conditions.
GEA Insights
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.
How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
