
Freeze Concentration, among all available concentration methods, provides the highest selectivity in water removal since ice crystals contain only water.
The complete separation of these ice crystals results in specific removal of water at very low processing temperatures. The very gentle concentration at sub-zero temperatures allows product freshness to be maintained and practically eliminates all biological degradation.
Since the crystallization process is highly specific for water and no vapor phase is present, all volatile aromas and flavors will be preserved in the liquid concentrate.
Key features:
- No loss of volatiles or solids
- Sub-zero temperature processing
- Maintains original product characteristics
- Closed system that prevents oxidation
- Elimination of microbiological activity
- Continuous and stable operation
What differentiates Freeze Concentration for food solutions from Melt Crystallization for chemicals is that the liquid is a solution with water instead of a chemical and the product is the concentrate instead of the separated (ice) crystals.
Freeze Concentration plants can be found in installations around the globe, with dewatering capacities ranging from 200 to 200,000 tons per year and handling a variety of products, from small volume specialties to large scale commodities, serving to diverse industrial processes that can be differentiated in two big groups:
Food concentrates
- Fruit juices, cider, wine, milk, whey, buttermilk,
- Coffee extract, tea extract, seaweed extract, fish extract
- Vinegar, wort
- Egg white liquid
Wastewater
- High purity water production from mixed wastewaters
- Separation from pure water from a feed containing dissolved volatile substances in a single step.
- Insensitivity to the presence of scaling components
- Insensitivity to the present of some suspended solids
- Handling of precipitating solids in a separate stream as a sludge (eutectic freeze concentration)
Products
Showing 3 of 3

Freeze Concentration Test Center
Available for detailed tests based on the feed properties and every product's requirements.

IceCon®
GEA's patented unique solid-liquid separation solution for Freeze Concentration.

IceCon® Compact
Standard skid mounted units suitable for the production of liquid food concentrates. All relevant components for running a freeze concentration plant.

Want to learn even more?
Webinar: Freeze concentration
- Explore GEA's technical expertise spanning over 60 years, featuring global installations and testing options.
- Learn about the IceCon® Compact series designed for straightforward installation, CODEX® automation for reliable operation, and upgrade services that reduce energy consumption by up to 30%.
- Review real-world application examples and case studies.
Downloads

GEA Insights
The breakthrough that changed spray drying
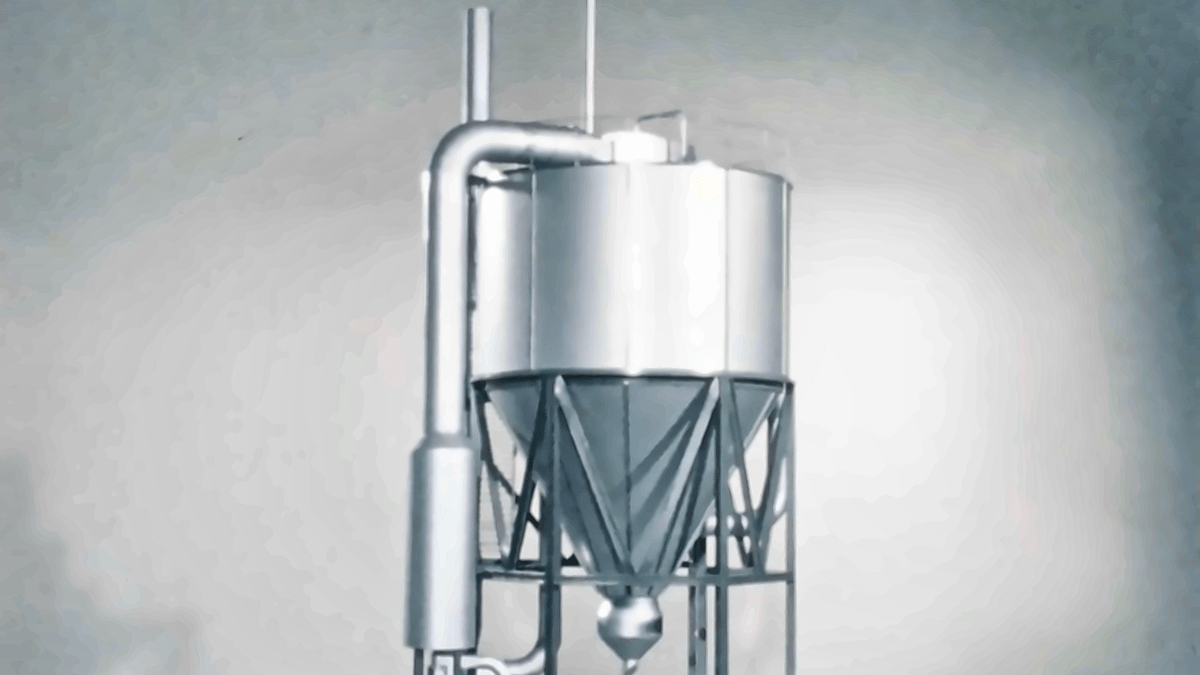
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.
How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
