

Die Batch-Destillation ist sehr flexibel, wird aber in der Regel nur für kleine und mittlere Kapazitäten eingesetzt. Bei größeren Kapazitäten ist eine Anlage zur kontinuierlichen Destillation normalerweise energieeffizienter und wirtschaftlicher.
Die Batch-Destillation kann in zwei Betriebsarten gefahren werden:
- Bei einer Batch-Destillation mit einem festen Rücklaufverhältnis werden die Verbindungen nach einem definierten, produktspezifischen Zeitplan getrennt. Die Basis für eine Fraktionierung sind die verschiedenen Siedepunkte der in Lösung vorliegenden Produkte: beginnend mit den Leichtsiedern und am Ende mit den Schwersiedern. Die klassische Anwendung ist die Fraktionierung von Gemischen mit unterschiedlichen Komponenten.
- Die Batch-Destillation mit einem variierenden Rücklaufverhältnis ermöglicht eine konstante Konzentration des Destillats. Dieses Prinzip wird immer dann angewendet, wenn ein Destillat mit konstanten physikalischen Verhalten erwünscht wird.
Batch-Destillationen werden häufig in der pharmazeutischen Industrie für kleine Anwendungen zur Lösungsmittel-Rückgewinnung, für die Aufreinigung von hoch wertvollen Ölen oder, in kleinerem Umfang, auch in Anlagen zur Abwasseraufbereitung eingesetzt,.

Key applications
Food, beverage and ingredients
Solvent recovery and recycling
Chemical product purification
Flavors, fragrances and essential oils
Pharmaceutical manufacturing
Bio-based chemicals

Downloads
Verwandte Produkte

Dehydrierung und Reinigung
Wenn höhere Produktkonzentrationen erforderlich sind, als durch Gegenstromdestillation gewonnen werden kann, kommen folgende Technologien zum Einsatz: Molekularsiebtechnik, Destillation mit Schleppmittel und Pervaporation durch hydrophile Membranen.

Kolonnenheizkörper für Destillationsanlagen
GEA verwendet unterschiedliche Heizkörpertypen für die Beheizung von Destillationskolonnen. Die Wahl des entsprechenden Typs hängt vom Prozessumfeld und den Produktparametern ab.

MBV/TBV-beheizte Destillationsanlagen
Bei der thermischen Brüdenverdichtung werden Dampfstrahlverdichter verwendet, um das Druck-/Temperaturniveau der Brüdenströme in der Anlage zu erhöhen. Die Kondensationsenthalpie dieser im Druck angehobenen (komprimierten) Brüdenströme wird anschließend für die Beheizung von Verdampfungsprozessen verwendet, die auf einem tieferen Temperaturniveau...

Prozessintegration
Produktionslinien mit optimierten Prozessschritten.
GEA Insights
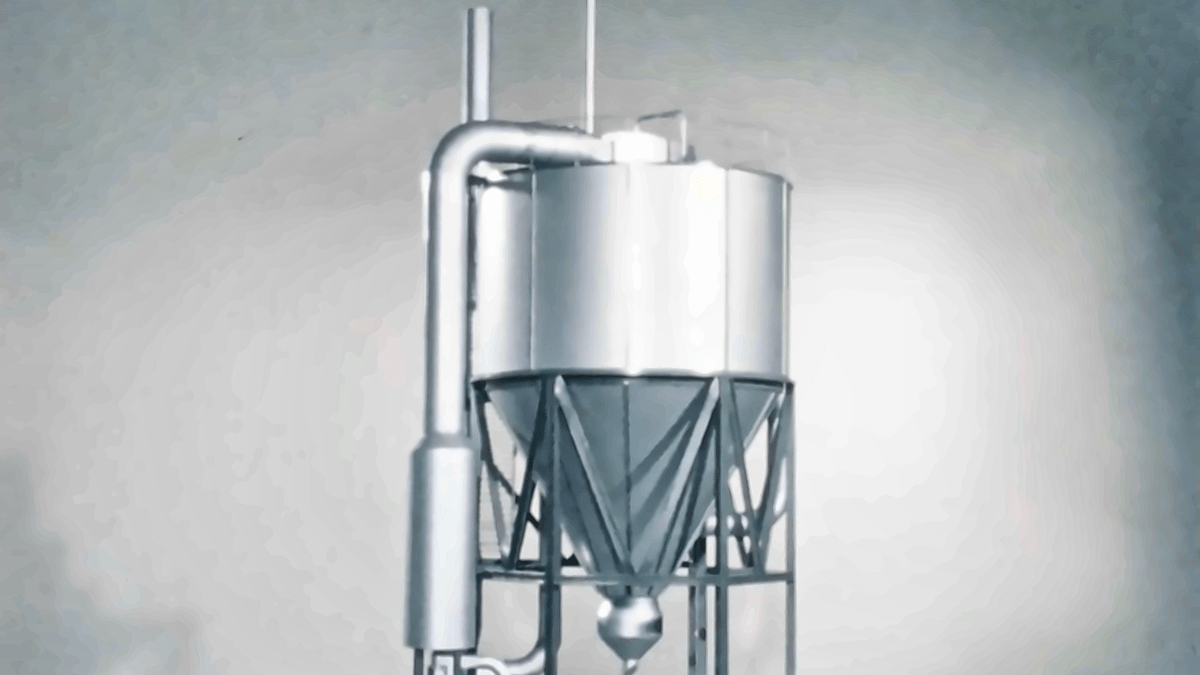
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
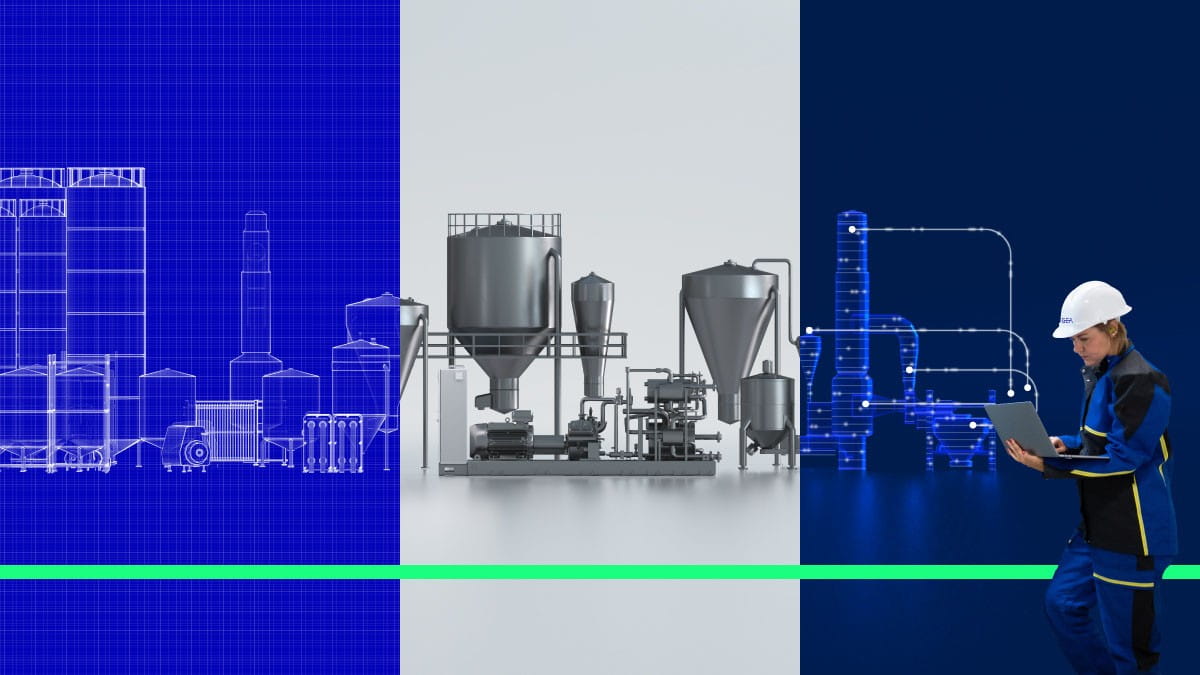
Das Ganze im Blick: Wie Anlagen dauerhaft besser laufen
Eine effiziente Maschine macht noch keine effiziente Produktion. Echte Verbesserungen beginnen oft damit, den Blick über die einzelnen Anlagenelemente hinaus zu richten und zu verstehen, wie sich Prozesse, Energiesysteme und betriebliche Entscheidungen gegenseitig beeinflussen. Ein solcher ganzheitlicher Ansatz hilft beim Identifizieren von Potenzialen, die sonst verborgen bleiben.
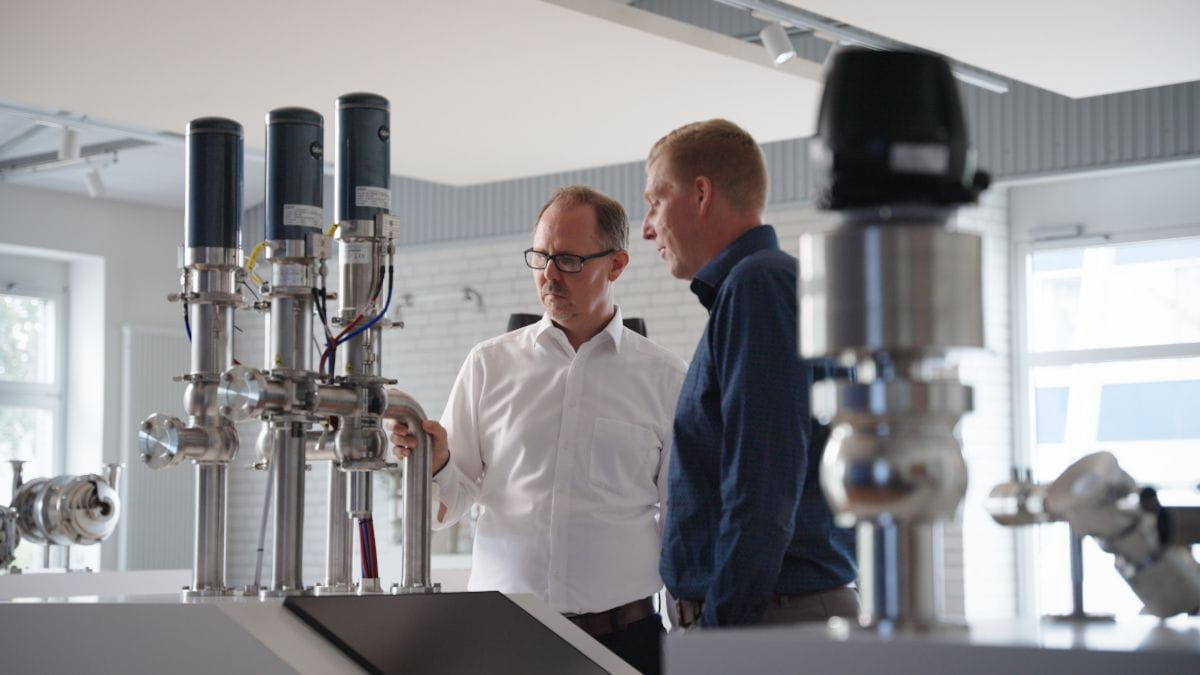
Wie eine neue Ventiltechnologie die Produktion von Lebensmitteln und Getränken verändert
In der Lebensmittel- und Getränkeindustrie werden Ventile traditionell mit Druckluft betrieben. Die GEA Hydract®-Antriebstechnologie betätigt Ventile dagegen mit Wasser in einem geschlossenen, digital gesteuerten Kreislauf. Das Ergebnis: Ventile lassen sich präzise in jeder gewünschten Position halten und in fein abgestuften Schritten steuern. Dadurch sinken der Energieverbrauch und gleichzeitig steigt die Prozesskontrolle erheblich.
