


Increase your DCO recovery rates: 3-phase decanters from GEA with Varipond C
Why Choose a 3‑Phase Decanter for DCO Recovery?
1. High Corn Oil Yield from Whole Stillage
3‑phase decanters separate solids, water, and oil in a single, continuous step, making it ideal for recovering corn oil before the actual stillage decanter, or after the evaporation stage.

3-phase decanters separate the whole stillage into DCO, thin stillage and wet distillers grain in one single step.
2. Stable Performance — Even with Process Variability
Stillage composition can vary with upstream fermentation conditions, grind quality, or enzyme performance. A 3‑phase decanter is engineered to handle these fluctuations, maintaining stable dryness, oil separation efficiency, and centrate clarity. The result: consistent DCO recovery, day after day.
3. Lower Energy Consumption in Downstream Processes
By removing more free and emulsified oil early, the remaining thin stillage requires less energy in evaporation and produces a more stable syrup (CDDGS/DDGS). Improved phase separation also reduces load on downstream disk stack centrifuges - cutting energy use and extending equipment life.
4. Maximum Flexibility for Bioethanol Plant Operations
3‑phase decanters integrate seamlessly into both new and existing bioethanol plants. They can be configured to recover oil from whole stillage, thin stillage or syrup and work as the primary or secondary oil recovery step. This flexibility makes it easy to tailor the system to plant capacity, oil yield targets, and process layout.
5. High-Quality Corn Oil Output
With precise control of differential speed, pond depth, and feed conditioning, a 3‑phase decanter produces a clean oil phase with lower moisture and solids. Higher oil purity means better market value and improved downstream handling.
Speaking of control
GEA Varipond C
With GEA Varipond C adjusting your 3-phase decanters to changing feed conditions, flow rates or even feedstocks can be done instantly and directly at the running machine. Just select the respective diameter and the position of the centripetal pump adjusts the separation zone inside the bowl.
It is easy, fast, precise and even easily repeatable if saved as recipe in your control system.
Key benefits for 3-phase DCO and stillage decanters
- Higher DCO recovery from stillage
- Reduced energy costs in evaporation
- Improved DDGS quality thanks to less residual oil
- Stable performance under variable plant conditions
- Robust, low-maintenance design for 24/7 operation
- Optimized integration with existing plant equipment
Boost Revenue and Efficiency with a 3‑Phase Decanter
Whether your goal is to increase corn oil yield, reduce operational costs, or optimize the entire coproduct stream, a 3‑phase decanter delivers measurable advantages across the bioethanol process. By adding this technology, plants can extract more value, improve sustainability metrics, and strengthen overall profitability

GEA Insights
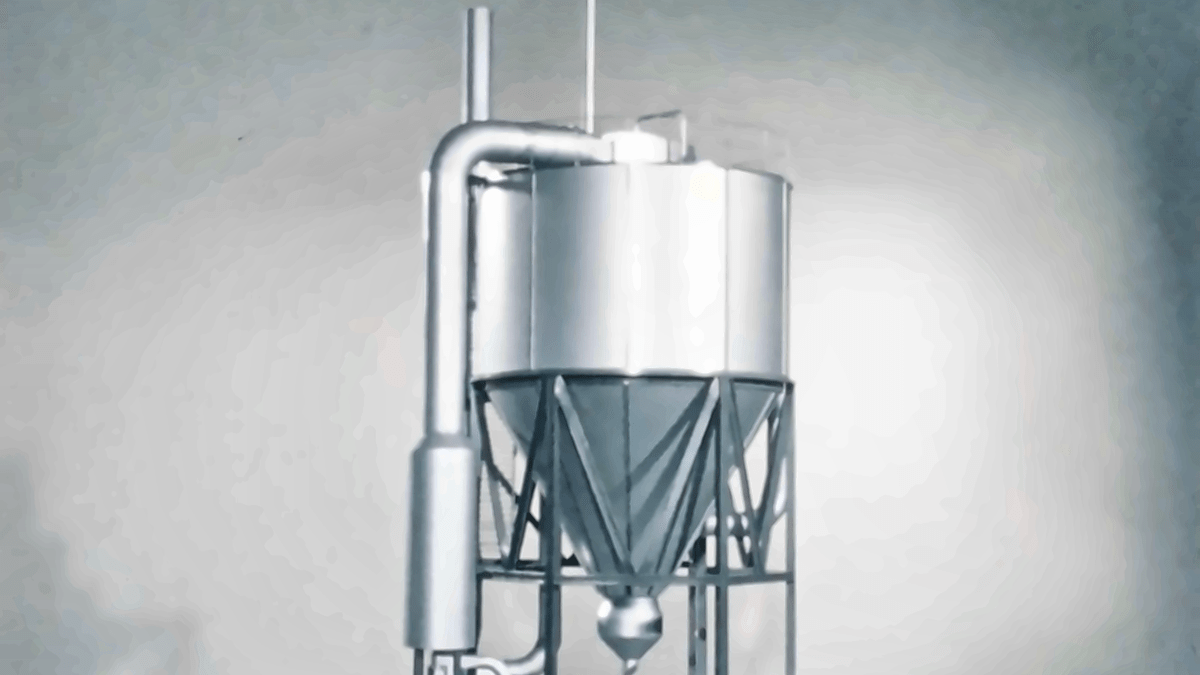
El avance que revolucionó el secado por atomización
En 1976, los ingenieros de NIRO respondieron a un reto competitivo replanteándose las posibilidades del secado por atomización. Su idea se materializó en la torre multietapa MSD. Cincuenta años después, ese mismo principio fundamental contribuye a transformar los líquidos en los productos en polvo que se utilizan en productos nutricionales esenciales y en medicamentos importantes en todo el mundo. Perfeccionada a lo largo de décadas de experiencia en ingeniería, conocimiento de las necesidades de los clientes y desarrollo continuo, la torre de atomización MSD es una historia de innovación con un impacto duradero.

Más allá de la máquina: cómo potenciar el rendimiento de la planta
El hecho de que una máquina sea eficiente no significa que la fábrica lo sea. La mejora real suele comenzar por ir más allá de los equipos individuales y comprender cómo los procesos, los sistemas energéticos y las decisiones operativas se influyen mutuamente. Se trata de un enfoque holístico diseñado para descubrir oportunidades que, de otro modo, podrían pasarse por alto.

Cómo una válvula transforma la manera de elaborar alimentos y bebidas
En las plantas de alimentación y bebidas, las válvulas suelen accionarse mediante aire comprimido. GEA Hydract® Actuation Technology mueve las válvulas mediante agua, en un circuito cerrado controlado digitalmente. El resultado es una válvula que puede mantenerse en su sitio con exactitud y regularse con precisión. Esto se traduce en un menor consumo energético y un mayor control.
