
Powder sampling is an important part of any quality assurance process in a food plant. The samples taken are typically used to check for process conformity, or for defects such as composition and bacteriological contamination.
When sampling product for quality testing it is important that the sample reaches the storage container without being damaged. Samples taken directly from the powder storage hopper must be discharged close to the sampling point.Products
Showing 4 of 4

GEA Powder Sampler (PAS)
GEA powder samplers have been designed to complement the powder filling systems we supply. Our auger sampler can take representative powder samples at the point where the powder enters the bag even when packing in inert atmosphere conditions.

GEA Powder Spool Sampler
The GEA Powder Spool Sampler is a low cost hygienic solution for reliable and remote powder sampling designed specifically for Dairy and Food processors. The simple design provides a robust method for taking fixed volume powder samples at any point in the powder manufacturing process
Powder Sampling for Contained Systems
GEA offers a range of contained sampling devices for the pharmaceutical industry. These devices are build around the Buck® valve technologies.

Vacuum Powder Sampler
GEA manufactures a range of sampling systems to suit sanitary applications, we use dynamic sampling. Superior methods of powder sampling are obtained by using procedures where the sample is removed from a moving powder bulk.
Downloads
GEA Insights
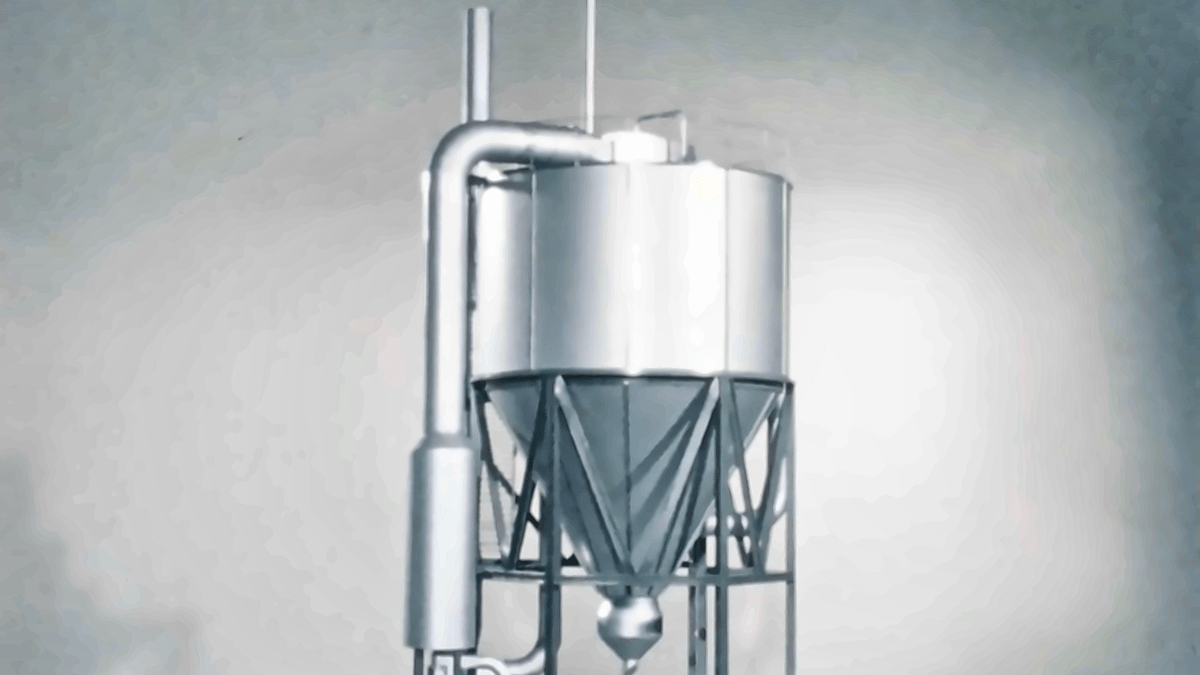
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.
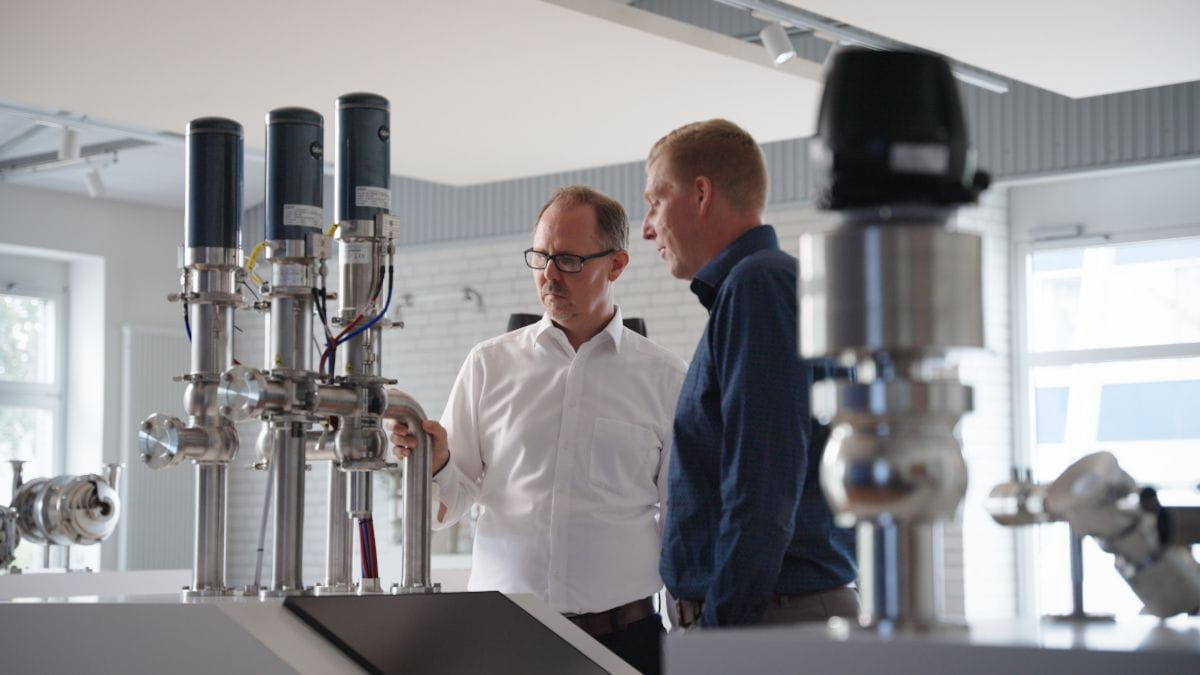
How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
