

Tubular heat exchangers are essential components in various industrial processes, enabling efficient heat transfer between two fluids or gases. They are critical for maintaining optimal temperatures, improving energy efficiency, and ensuring smooth system operations.
As a manufacturer, staying competitive means relying on equipment, recipes, and processes that ensure hygienic, efficient, and reproducible production while delivering products with the desired properties and functionality.
Our heat exchangers are designed to meet these demands. Tailored to your specific application, it offers a customized solution to ensure top performance and reliability.
Tubular Heat exchangers for product heating
We offer a diverse portfolio of tubular heat exchanger modules for a wide range of products, that require to be heated, cooled or pasteurized.
The most appropriate design can be selected depending on the required production capacity and the physical properties of the product. Custom designs can also be developed and installed to suit highly specialized applications. The GEA VARITUBE® heat exchangers meet aseptic standards and are available for liquid food, liquid dairy products, beverages and new food.
Tubular heat exchangers for energy & utilities
Our standardized utility heat exchangers are available in different construction shapes and predefined sizes, with the focus to meet a high variety of water or CIP heating applications.
Products
Showing 2 of 2

GEA VARITUBE® Tubular Heat Exchangers for energy & utilities
Multitube with indirect heat exchange, suitable mainly for hot water generation and heating of CIP media with steam or hot water.

GEA VARITUBE® Tubular Heat Exchangers for product heating
Our GEA VARITUBE® range is used for many products that need to be heated, cooled or pasteurized.
Downloads

GEA Insights
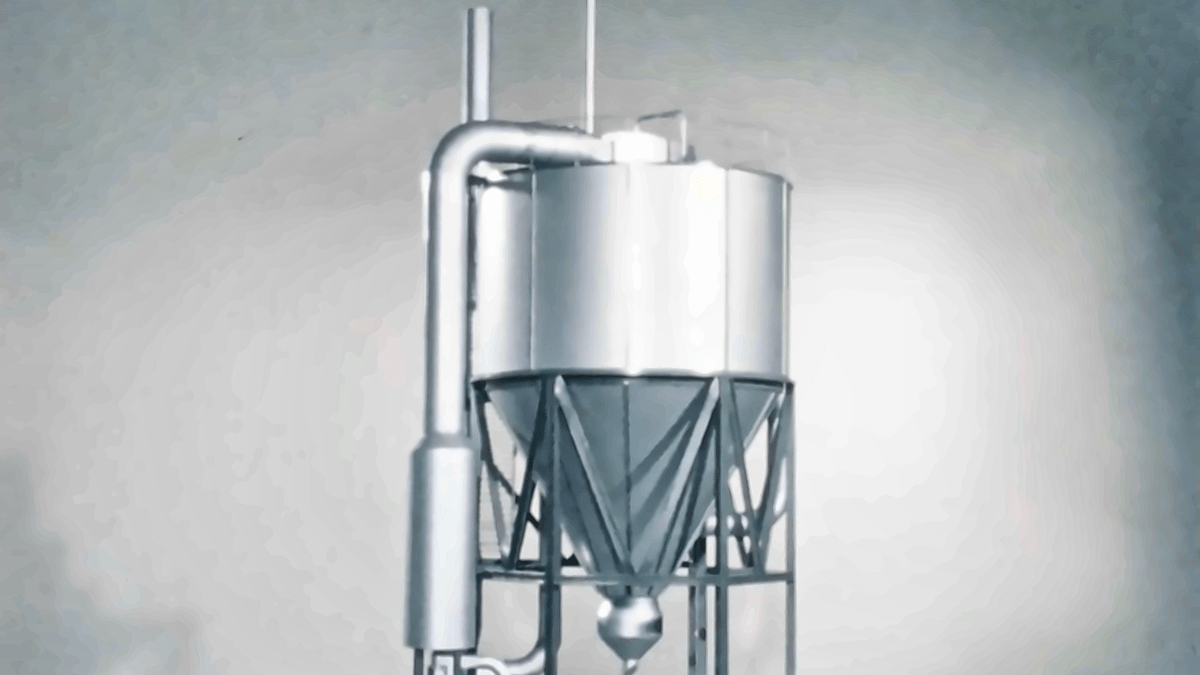
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.

Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.

How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
