

Fuel quality can vary significantly, particularly when operating with heavy fuel oil. Differences in viscosity, temperature and pressure can affect engine performance, efficiency and reliability if fuel properties do not match the engine manufacturer's specifications.
The GEA Visco Booster Unit (VBU) automatically conditions fuel between the fuel supply system and the engine, continuously adjusting viscosity, temperature and pressure to the required operating parameters. The result is stable engine performance, improved fuel compatibility and reliable operation across varying fuel qualities.
Designed to meet different engine manufacturer requirements, the VBU is available in multiple system configurations for single or multiple engines, with optional standby functions for pumps and preheaters. Its compact design, high-quality components and simplified maintenance make it an ideal solution for both newbuild and retrofit projects.
Features
Precise fuel conditioning
Automatically adjusts fuel viscosity, temperature and pressure to match engine specifications, ensuring stable and efficient engine operation.
Reliable operation with varying fuel qualities
Compensates for differences in heavy fuel oil and other marine fuels, delivering consistent fuel quality and dependable engine performance.
Flexible configurations for every application
Available in multiple system variants for one or more engines, with optional standby functions for feeder pumps, booster pumps and heavy fuel oil preheaters to meet different engine manufacturer requirements.
Compact and easy to integrate
Designed for straightforward installation, simplified maintenance and optimal use of available space in both newbuild and retrofit projects.
Engineered for long-term reliability
High-quality components, optimized system design and continuous operation ensure dependable performance and a long service life in demanding marine environments.
Downloads
Related Products

GEA methanol Fuel2Engine System
GEA methanol Fuel2Engine System combines Booster Unit and Valve Train for reliable methanol fuel conditioning and engine injection.

Separators for Marine
Marine separators specialize in the purification of fuel and lube oil as well as bilge and EGR water treatment on board ships.

GEA biofuel Separator
GEA biofuel Separators are tailored to the specific characteristics of biofuels, efficiently separating water and contaminants to meet the stringent requirements of the industry.

GEA ecomarine Separator
The GEA ecomarine Separator is an energy-efficient solution for lube oil treatment and a cost-effective alternative to traditional filter systems.
GEA Insights
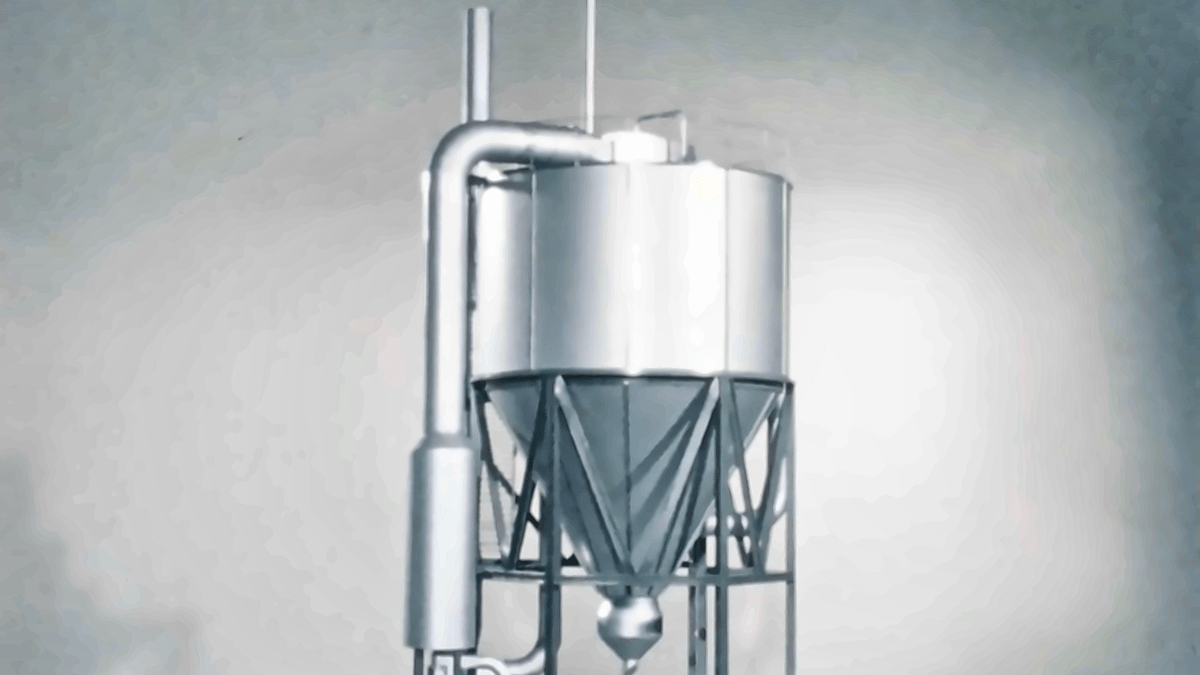
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.

Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.

How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
