

GEA Kob® is the cost-efficient line of homogenizers and high-pressure pumps designed to bring industrial-grade performance to small and mid-sized manufacturers in a broad range of industries and applications. Engineered to meet the needs of customers seeking efficient homogenization and automation solutions, Kob® homogenizers provide flexibility, easy installation, and exceptional value for money.
Why choose Kob® homogenizers and high-pressure pumps?
Kob® homogenizers and high-pressure pumps combine reliable quality and competitive pricing, thanks to significant investments in optimized design, engineering, supply chain management, and manufacturing processes. The range is designed with simplicity in mind, featuring a low number of parts, ease of use, and minimal maintenance requirements. With their compact size, Kob® machines are perfect for industries where space is limited.
High operating pressure – up to 400 bars
Kob® homogenizers operate at pressures up to 400 bars, making them suitable for nearly all dairy, food and beverage applications and for some chemical, cosmetic, and personal care applications – including moderately viscous and abrasive formulation and spray dryers, allowing for versatile use across various industries.
Full range of homogenizing valves
- The basic machine uses competitively priced wear-resistant parts, ideal for non-abrasive applications.
- Optional high-wear-resistant materials extend service life in more demanding, abrasive formulations.
- Optional higher-efficiency homogenizing valves are also suitable.
- GEA coneVerge® for ultra-low pressure efficiency, especially designed for dairy and beverage applications.
- GEA NanoValve® for high efficiency in medium-pressure applications.
New frame and cladding design
- All stainless-steel construction engineered with advanced tools for a robust structure and long-term durability.
- Optimized crankcase for low mechanical heat generation, noise and vibrations.
- No need for cooling lubrication oil or forced air ventilation in the drive compartment.
Poppet pumping valves
- Excellent flow characteristics with easy feeding and reduced noise and cavitation.
- High volumetric efficiency and extended operational life.
Compact footprint
- Optimizes plant space while allowing easy replacement of old homogenizers.
- Minimal space required for maintenance.
Hygienic design
- CIP (Clean in Place) capable.
- Optional 3A approval for enhanced hygienic standards.
Aseptic execution
- Simple operation and control for long-lasting plunger and seal performance.
- All parts in contact with the product are SIP (Sterilize in Place) capable.
- Steamable full stroke barrier chambers for extra hygiene.
Flexible electrical and automation options
- A wide range of electrical options and automation levels to suit different control needs, from basic motor starter panels to high-spec PLC panels with HMI.
- Profinet communication options for integration with central PLC/SCADA systems.
- This modularity ensures fast installation as well as smooth retrofitting into existing production lines.
All this makes Kob® homogenizers a reliable, high-performing, resource-efficient and cost-effective solution for a wide range of industries. If you're looking for high-quality homogenizers and pumps that deliver outstanding performance while saving space and maintenance costs, Kob® is your ideal choice.
| Models | Kob® Homogenizer 11 | Kob® Homogenizer 22 | Kob® Homogenizer 45 | Kob® Homogenizer 90 |
|---|---|---|---|---|
| Max Capacity (l/h) | 2,200 | 5,000 | 9,700 | 18,000 |
| Max Pressure (bar) | 400 | 400 | 400 | 400 |
Verwandte Produkte

GEA Ariete Homogenisator 5400
Der Ariete Homogenisator 5400 bietet die umfangreichste, jemals erreichte Kapazität (80.000 l/h bei 120 bar) und die größte Vielseitigkeit: von der Milch- und Getränkebranche bis zur pharmazeutischen und chemischen Industrie, wobei maximale Effizienz und Betriebssicherheit gewährleistet werden.

Hochdruckpumpen - Baureihe Ariete
Hochdruckpumpen sind ideal für die Übertragung von Flüssigkeiten in industriellen Anlagen, und besonders für viskose Produkte.

Homogenisatoren Baureihe One
Die Baureihe One kann jede Herstellungsanforderung für kleine und mittlere Herstellungen erfüllen. Sie bietet eine einfache Konstruktion, mit allen Optionen, die für eine einfache Integration in ein bestehendes System erforderlich sind, ist betriebsbereit und hat nur wenige Wartungseinheiten.

O.P.S. Ölreinigungssystem
Das Ölreinigungssystem (O.P.S.) ist die Bypass-Filtrationseinheit zur Wahrung einer hohen Ölqualität und für die Garantie einer kontinuierlichen Ölregeneration durch die Entfernung von Partikeln, Wasser, korrosiven Gasen und Verunreinigungen; auf diese Weise werden Lebensdauer, Qualität und Sicherheit erhöht.
GEA Insights
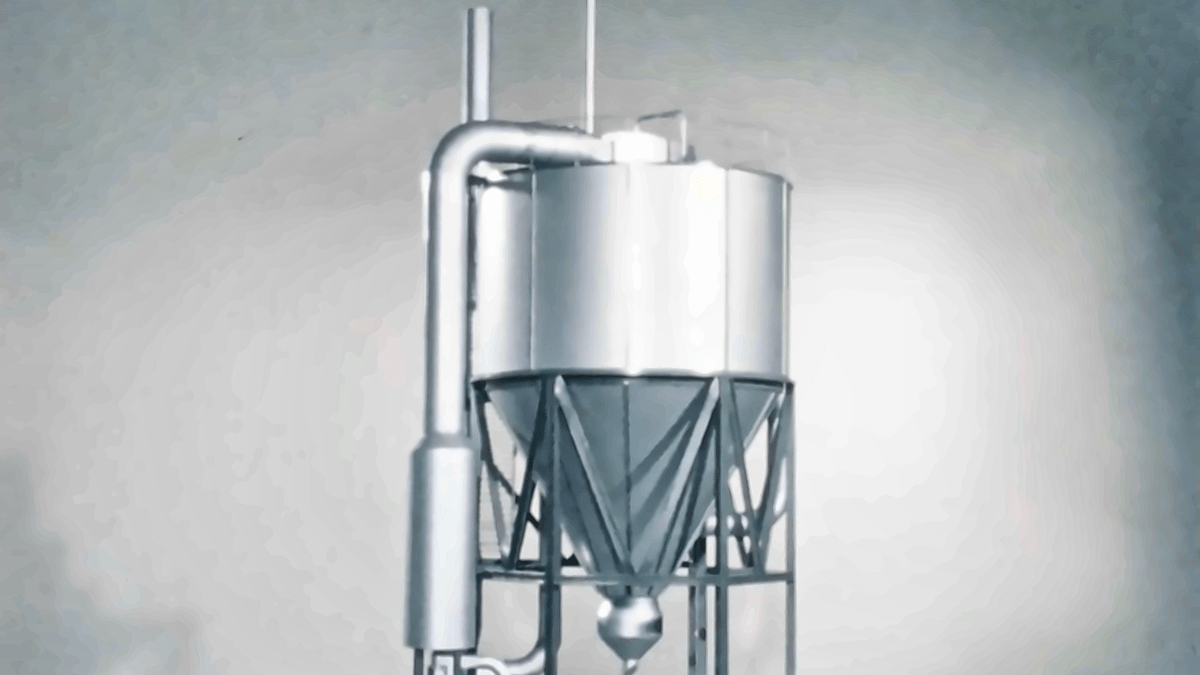
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.

Das Ganze im Blick: Wie Anlagen dauerhaft besser laufen
Eine effiziente Maschine macht noch keine effiziente Produktion. Echte Verbesserungen beginnen oft damit, den Blick über die einzelnen Anlagenelemente hinaus zu richten und zu verstehen, wie sich Prozesse, Energiesysteme und betriebliche Entscheidungen gegenseitig beeinflussen. Ein solcher ganzheitlicher Ansatz hilft beim Identifizieren von Potenzialen, die sonst verborgen bleiben.

Wie eine neue Ventiltechnologie die Produktion von Lebensmitteln und Getränken verändert
In der Lebensmittel- und Getränkeindustrie werden Ventile traditionell mit Druckluft betrieben. Die GEA Hydract®-Antriebstechnologie betätigt Ventile dagegen mit Wasser in einem geschlossenen, digital gesteuerten Kreislauf. Das Ergebnis: Ventile lassen sich präzise in jeder gewünschten Position halten und in fein abgestuften Schritten steuern. Dadurch sinken der Energieverbrauch und gleichzeitig steigt die Prozesskontrolle erheblich.
