

Efficient conversion of sugars into ethanol.
GEA combines fermentation know-how with advanced process engineering to support reliable, large-scale ethanol production.
During fermentation, fermentable sugars are converted into ethanol using controlled yeast propagation and precise process control. GEA supports customers with process integration, equipment selection, and plant design to support alcohol yield, stable operation, and efficient downstream processing.
Key benefits
- High ethanol yield
- Stable fermentation performance
- Optimized yeast utilization
- Reduced contamination risks
From feedstock preparation and fermentation to ethanol purification, coproduct recovery, and energy optimization, GEA delivers integrated ethanol production solutions designed to support yield, reduce energy demand through process integration, and enable biofuel manufacturing.
Fermentation process
Ethanol production from starch- or sugar-based feedstocks is one of the oldest forms of value-added agricultural processing.
While the basic principle remains the same, modern ethanol production has evolved into a integrated biorefinery process. Today’s renewable fuel plants use advanced technologies to convert grains, sugar-based crops, beverage and food waste, cellulosic biomass, and other feedstocks into high-quality ethanol and valuable coproducts.
In a typical process, enzymes convert starch into fermentable sugars. The mash is cooked, cooled, and transferred to fermenters, where yeast initiates the conversion of sugar into ethanol. After fermentation, the resulting beer is separated from the remaining stillage. The ethanol is then distilled, dehydrated, and—where required for fuel applications—denatured before shipment. The stillage can be further processed to recover solids, soluble, distillers grains, and corn distillers oil.

Key process steps
Mash cooling & Preparation
Yeast propagation
Main fermentation
Fermentation temperature control
Carbon dioxide generation and recovery
Transfer to distillation
How does ethanol fermentation work?
Explore the key steps of ethanol fermentation with GEA process expertise.
Ethanol fermentation converts fermentable sugars into alcohol through controlled biological processes. GEA supports this conversion with integrated engineering, fermentation system design, yeast management, temperature control, separation technologies, and downstream process integration to help producers achieve stable and efficient ethanol production with integrated energy recovery options.
Why partner with GEA for ethanol fermentation?
Process expertise across the complete ethanol production chain.
GEA combines fermentation know-how with process engineering, separation technology, evaporation, drying, and energy integration to support efficient ethanol production from a wide range of feedstocks.
Customers benefit from:
- Integrated plant design from mash preparation to ethanol purification.
- Optimized fermentation conditions for high yield and stable operation.
- Reliable yeast propagation, cooling, and process control concepts.
- Efficient separation and clarification to protect downstream distillation performance.
- Energy-efficient technologies designed to support optimized steam consumption and help manage operating costs.
- Global engineering, project execution, and lifecycle service support.
Whether you are planning a new bioethanol plant, expanding existing capacity, or optimizing fermentation performance, GEA can develop a process concept tailored to your feedstock, production goals, and energy requirements.
By combining fermentation, separation, thermal concentration, and energy recovery technologies, GEA helps ethanol producers improve yield, manage resource consumption and support overall plant profitability.
Benefits for ethanol producers
- High ethanol yield and consistent product quality.
- Stable fermentation performance and reduced contamination risk.
- Integrated heat recovery concepts that help reduce overall energy demand across the process.
- Coproduct recovery with optional resource recovery benefits.
- Reduced operating costs and improved use of energy and coproduct streams.
Looking to optimize your ethanol fermentation process?
Contact GEA’s ethanol process experts to learn how integrated fermentation, separation, and energy recovery solutions can help improve yield and efficiency and integrate energy and coproduct recovery in ethanol production.
Downloads
Verwandte Produkte
Batch-Destillationsanlagen
Batchbetriebene Einheiten ermöglichen die Destillation und Rektifikation von verschiedenen Produkten oder mehreren Mischungen in nur einem Gerät. Somit ist die Batch-Destillation eine sog. Multi-Tasking Anwendung.

Continuous distillation
GEA designs and supplies advanced continuous distillation systems for the efficient separation and purification of liquid mixtures. Combining deep process expertise with proven thermal technologies, we help customers achieve high product quality, reduced energy consumption, and reliable plant operation across chemical, pharmaceutical, bio-based, ...

Destillations-Versuchsanlagen im Forschungs- und Entwicklungszentrum in Karlsruhe
Unser Forschungs- und Entwicklungszentrum ist mit hochmodernen Versuchsanlagen und Prüfständen optimal für Tests im Bereich der Destillations-Technologie ausgerüstet.

Mehrstufige Destillationsanlagen
Das Herzstück unserer Produktpalette bilden mehrstufige (druck-/vakuumgestufte) Destillationsanlagen. Das verfahrenstechnische Konzept wird weitgehend durch die Produkteigenschaften des Feeds und den Anforderungen an das Endprodukt bestimmt.
GEA Insights
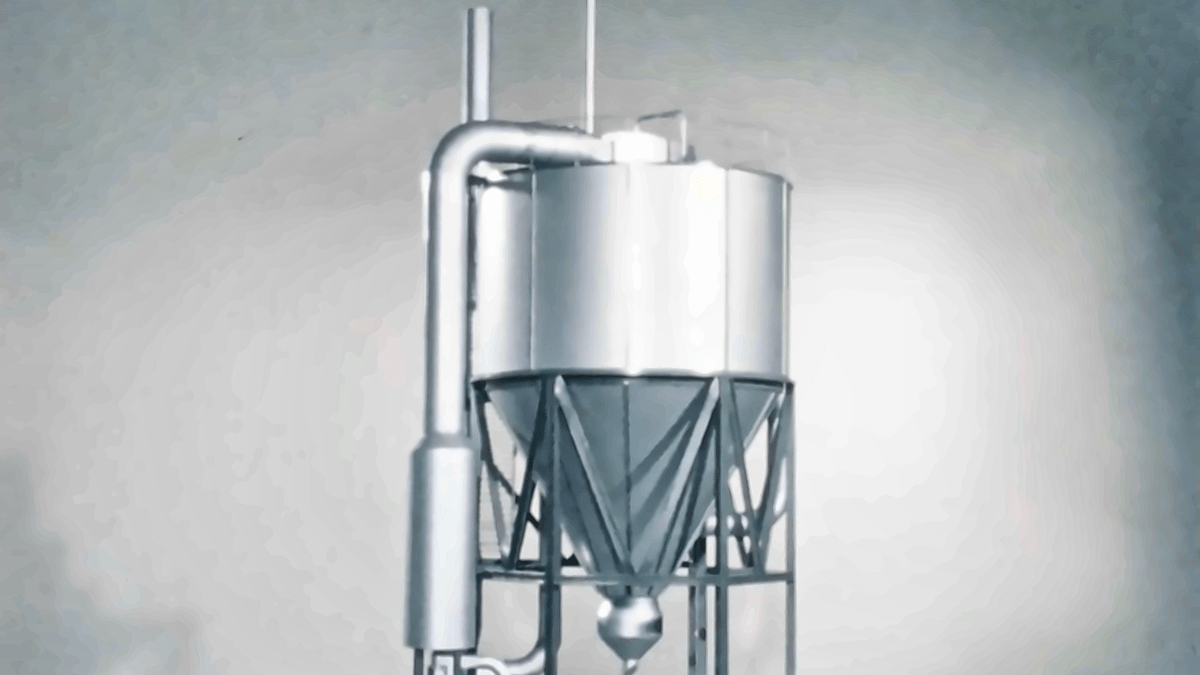
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Das Ganze im Blick: Wie Anlagen dauerhaft besser laufen
Eine effiziente Maschine macht noch keine effiziente Produktion. Echte Verbesserungen beginnen oft damit, den Blick über die einzelnen Anlagenelemente hinaus zu richten und zu verstehen, wie sich Prozesse, Energiesysteme und betriebliche Entscheidungen gegenseitig beeinflussen. Ein solcher ganzheitlicher Ansatz hilft beim Identifizieren von Potenzialen, die sonst verborgen bleiben.
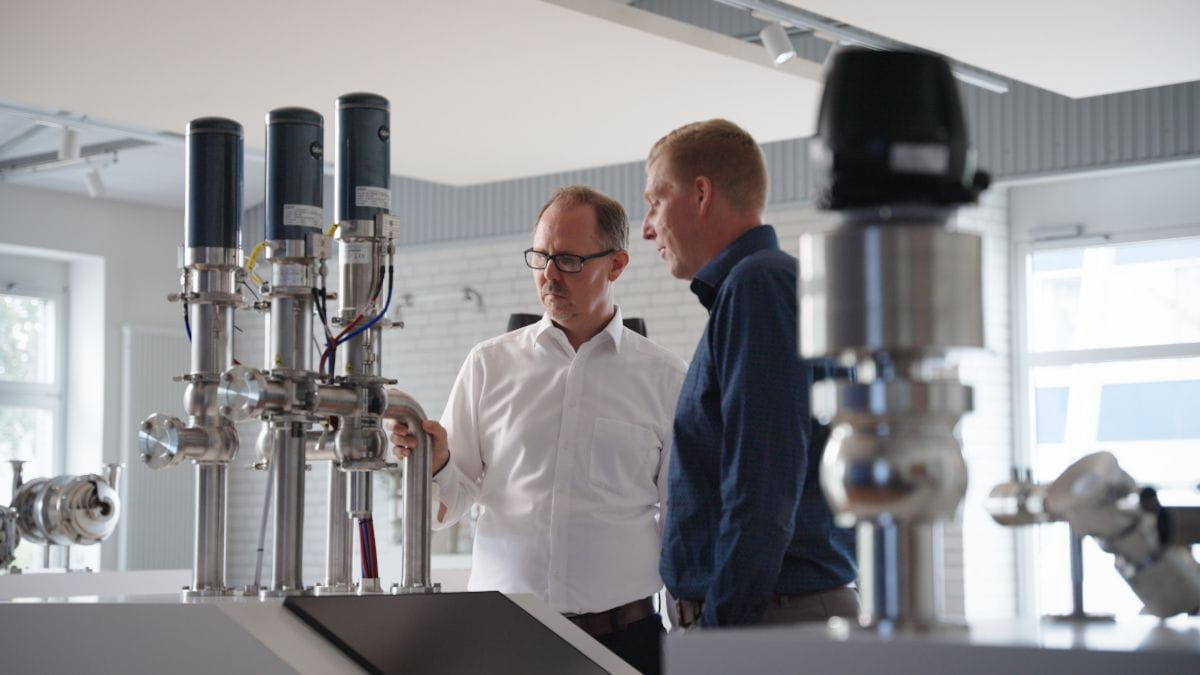
Wie eine neue Ventiltechnologie die Produktion von Lebensmitteln und Getränken verändert
In der Lebensmittel- und Getränkeindustrie werden Ventile traditionell mit Druckluft betrieben. Die GEA Hydract®-Antriebstechnologie betätigt Ventile dagegen mit Wasser in einem geschlossenen, digital gesteuerten Kreislauf. Das Ergebnis: Ventile lassen sich präzise in jeder gewünschten Position halten und in fein abgestuften Schritten steuern. Dadurch sinken der Energieverbrauch und gleichzeitig steigt die Prozesskontrolle erheblich.
