


Increase your DCO recovery rates: 3-phase decanters from GEA with Varipond C
Why Choose a 3‑Phase Decanter for DCO Recovery?
1. High Corn Oil Yield from Whole Stillage
3‑phase decanters separate solids, water, and oil in a single, continuous step, making it ideal for recovering corn oil before the actual stillage decanter, or after the evaporation stage.

3-phase decanters separate the whole stillage into DCO, thin stillage and wet distillers grain in one single step.
2. Stable Performance — Even with Process Variability
Stillage composition can vary with upstream fermentation conditions, grind quality, or enzyme performance. A 3‑phase decanter is engineered to handle these fluctuations, maintaining stable dryness, oil separation efficiency, and centrate clarity. The result: consistent DCO recovery, day after day.
3. Lower Energy Consumption in Downstream Processes
By removing more free and emulsified oil early, the remaining thin stillage requires less energy in evaporation and produces a more stable syrup (CDDGS/DDGS). Improved phase separation also reduces load on downstream disk stack centrifuges - cutting energy use and extending equipment life.
4. Maximum Flexibility for Bioethanol Plant Operations
3‑phase decanters integrate seamlessly into both new and existing bioethanol plants. They can be configured to recover oil from whole stillage, thin stillage or syrup and work as the primary or secondary oil recovery step. This flexibility makes it easy to tailor the system to plant capacity, oil yield targets, and process layout.
5. High-Quality Corn Oil Output
With precise control of differential speed, pond depth, and feed conditioning, a 3‑phase decanter produces a clean oil phase with lower moisture and solids. Higher oil purity means better market value and improved downstream handling.
Speaking of control
GEA Varipond C
With GEA Varipond C adjusting your 3-phase decanters to changing feed conditions, flow rates or even feedstocks can be done instantly and directly at the running machine. Just select the respective diameter and the position of the centripetal pump adjusts the separation zone inside the bowl.
It is easy, fast, precise and even easily repeatable if saved as recipe in your control system.
Key benefits for 3-phase DCO and stillage decanters
- Higher DCO recovery from stillage
- Reduced energy costs in evaporation
- Improved DDGS quality thanks to less residual oil
- Stable performance under variable plant conditions
- Robust, low-maintenance design for 24/7 operation
- Optimized integration with existing plant equipment
Boost Revenue and Efficiency with a 3‑Phase Decanter
Whether your goal is to increase corn oil yield, reduce operational costs, or optimize the entire coproduct stream, a 3‑phase decanter delivers measurable advantages across the bioethanol process. By adding this technology, plants can extract more value, improve sustainability metrics, and strengthen overall profitability

GEA Insights
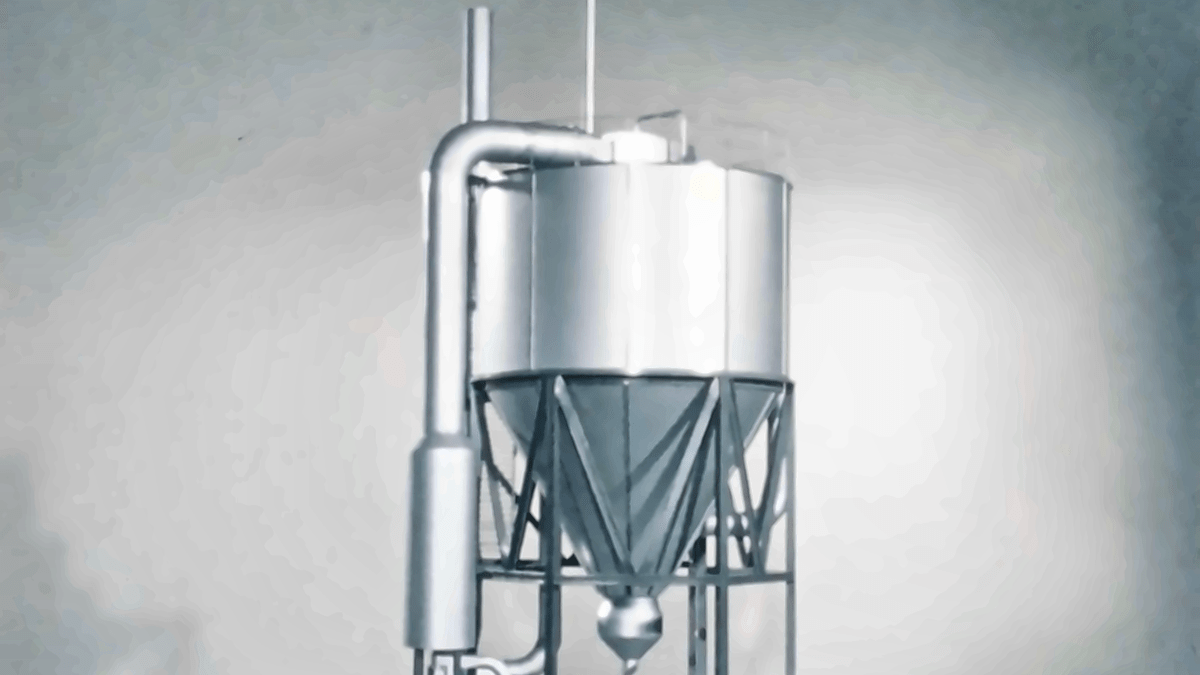
Przełom, który odmienił suszenie rozpyłowe
W 1976 roku inżynierowie NIRO odpowiedzieli na wyzwanie ze strony konkurencji, na nowo definiując możliwości suszenia rozpyłowego. Ich pomysł dał początek wielostopniowej suszarce MSD. Pięćdziesiąt lat później ta sama podstawowa zasada pomaga przekształcać płyny w proszki wykorzystywane na całym świecie do produkcji niezbędnych produktów żywieniowych i ważnych leków. Historia MSD, doskonalonej przez dziesięciolecia dzięki wiedzy inżynieryjnej, doświadczeniom klientów i ciągłemu rozwojowi, to historia innowacji o trwałym znaczeniu.

Więcej niż maszyna: klucz do poprawy wydajności zakładu
Wydajność maszyny nie przekłada się automatycznie na wydajność fabryki. Prawdziwa poprawa często zaczyna się od wyjścia poza ramy poszczególnych urządzeń i zrozumienia, w jaki sposób wzajemnie na siebie oddziałują procesy, systemy energetyczne i decyzje operacyjne. Jest to podejście kompleksowe, mające na celu odkrycie możliwości, które w przeciwnym razie mogłyby zostać przeoczone.

W jaki sposób zawór może wpływać na sposób produkcji żywności i napojów
Zazwyczaj w zakładach produkujących żywność i napoje zawory są uruchamiane za pomocą sprężonego powietrza. Tymczasem w GEA Hydract® Actuation Technology do sterowania zaworami wykorzystuje się wodę w zamkniętym obiegu sterowanym cyfrowo. W rezultacie otrzymujemy zawór, który można precyzyjnie utrzymać w odpowiednim położeniu i sterować nim z dużą dokładnością. Skutkuje to mniejszym zużyciem energii i większą kontrolą.
