

Reliable separation. Consistent purity. Designed to support lower energy demand.
Distillation remains one of the most important separation technologies in process industries. Whether the objective is solvent recovery, product purification, concentration, or the separation of complex compound mixtures, GEA delivers tailored continuous distillation solutions that support process performance while helping to control operating costs.
From conventional reboiler-driven systems to meVap® vapor recompression technologies designed to reuse process heat and multiple-effect concepts, our plants are engineered to meet demanding production requirements while supporting energy-efficiency targets and the potential reduction of energy-related carbon emissions. Continuous energy reuse and optimized heat integration can significantly lower steam consumption and operational expenditure.
From laboratory-scale production to full industrial manufacturing, our continuous distillation enable precise control of product quality, yield, and operating efficiency.
Why continuous distillation?
Continuous distillation offers significant advantages over batch processing for large-scale industrial production:
Key benefits
- Consistent product quality and purity
- High throughput and continuous operation
- Reduced operating costs
- Lower energy consumption through heat recovery
- Improved process control and automation
- Enhanced plant availability and reliability
GEA's process specialists design each distillation system according to the specific physical properties of the feed mixture and the desired product specifications, supporting reliable performance across the defined operating range.
Multiple-effect distillation
For applications requiring efficient thermal energy use, GEA offers multiple-effect distillation systems that repeatedly utilize supplied thermal energy across several effects.
By cascading energy from one effect to the next, steam demand can be reduced in relation to the number of effects applied. This can support energy-efficient operation and help reduce operating costs.
Key advantages
- Efficient thermodynamic performance
- Reduced utility consumption
- High product yield
- High distillate purity
- Proven technology for large-scale production environments
GEA meVap® Distillation
Continuous Recycling of Energy Streams. Energy costs are often the largest operating expense in a distillation process. GEA meVap® Distillation utilizes mechanical vapor recompression (MVR) technology to recover and reuse latent heat from process vapors.
Instead of rejecting valuable thermal energy to cooling systems, the vapor is compressed to a higher pressure and temperature level and reused as the primary heating source within the process.This reuses process heat and can reduce steam demand and operating costs, depending on the process configuration.
Benefits
- Reduced steam consumption through process heat reuse
- Lower CO2 emissions
- Reduced utility costs
- Gentle product treatment through low temperature differences
- Lifecycle cost benefits for suitable new installations and revamps

Key applications
Food, beverage and ingredients
Solvent recovery and recycling
Chemical product purification
Biofuel production
Pharmaceutical manufacturing
Biochemical and fermentation industries
Waste stream valorization and resource recovery
Polymer and plastics production
Chemical production with resource recovery
How does Continuous Distillation work?
Discover the art of whisky distilling with GEA’s Process Line Tour.
Join us for an exclusive tour of GEA’s whisky distilling process line and explore how our advanced technologies help producers craft exceptional whisky—from raw ingredients to refined spirit. Whether you're a seasoned distiller or just curious about the craft, this deep dive reveals the precision, efficiency, and passion behind the gold liquid.

Why partner with GEA?
GEA helps customers reduce environmental impact through innovative thermal process technologies by integrating Mechanical Vapor Recompression (MVR) and advanced Heat Recovery concepts.
Global expertise in thermal separation
With decades of experience in distillation, evaporation, and thermal separation technologies, GEA combines process know-how, engineering excellence, and innovative energy-saving solutions to deliver systems that maximize productivity and long-term value.
Our customers benefit from:
- Customized plant design
- Proven thermal separation expertise
- Advanced energy-saving technologies
- High product purity and yield
- Global lifecycle support
- Sustainable production solutions
Whether you need a pilot unit, a dedicated production plant, or a highly specialized purification system, GEA can provide a continuous distillation solution tailored to your process requirements. Designed for uninterrupted operation, continuous distillation systems deliver consistent product quality, high throughput, and excellent process efficiency, making them ideal for large-scale industrial applications.
GEA's expertise in energy-efficient process design and vapor recompression technologies enables the recovery and reuse of thermal energy throughout the distillation process. By minimizing steam consumption and reducing operating costs, these solutions support energy- and cost-efficient plant operation while maintaining high separation performance and product purity.
Looking to optimize your separation process?
Contact our distillation experts to discuss how a GEA continuous distillation system can support product quality, help reduce energy demand, and contribute to your energy and resource efficiency objectives.
Downloads
Prodotti correlati
Impianti di distillazione batch
I sistemi a batch consentono di distillare e rettificare vari prodotti o miscele multicomponente in una sola unità. Si tratta della migliore soluzione multitasking per le applicazioni nel settore della distillazione.

Impianti di prova per la distillazione nel centro di ricerca e sviluppo di Karlsruhe
Con impianti pilota e banchi di prova all'avanguardia il nostro centro di ricerca e sviluppo è attrezzato in modo ottimale per prove nel campo della tecnologia di distillazione.

Disidratazione e purificazione
Ove sono necessarie purezze del prodotto superiori alle concentrazioni ottenibili mediante rettifica, viene utilizzata una delle seguenti tecnologie: tecnologia del setaccio molecolare, distillazione con trascinatore e pervaporazione attraverso membrane idrofiliche.

Ethanol fermentation processes
GEA provides integrated process solutions for ethanol production, covering key stages from raw material preparation and fermentation to ethanol purification and coproduct processing. Drawing on extensive experience in fermentation, thermal separation, evaporation, drying, and energy integration, GEA supports producers in optimizing yield, managin...
Approfondimenti GEA
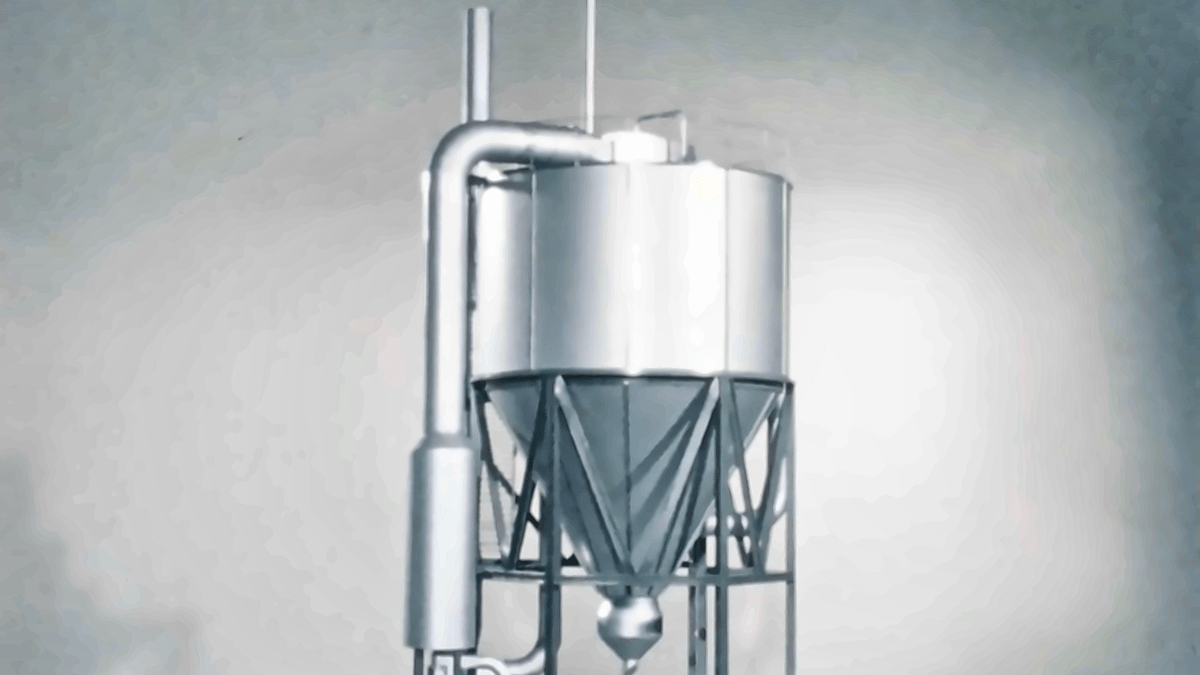
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Oltre le macchine: come migliorare le prestazioni dell’impianto
Una macchina efficiente non garantisce automaticamente l'efficienza di uno stabilimento. Il vero miglioramento spesso inizia guardando oltre le singole attrezzature e comprendendo come i processi, i sistemi energetici e le decisioni operative si influenzino a vicenda. Si tratta di un approccio olistico pensato per individuare opportunità che altrimenti potrebbero sfuggire.
Come una valvola rivoluziona la produzione di alimenti e bevande
Negli impianti di produzione di alimenti e bevande, le valvole vengono solitamente azionate tramite aria compressa. GEA Hydract® Actuation Technology utilizza l'acqua all'interno di un circuito chiuso e controllato digitalmente. Il risultato è una valvola che può essere mantenuta esattamente in posizione e regolata con per piccoli incrementi con grande precisione. Ciò si traduce in un minor consumo energetico e in un maggiore controllo.
