

Pasteurization is an essential step in manufacturing a wide range of liquid food products, such as ketchup, jam, mayonnaise, honey, and much more. And while every manufacturer expects their pasteurization systems to provide safe, effective heat treatment, here at GEA we also know that every customer will have different needs.
Tailor made for your processes
Built on decades of GEA expertise in liquid food processing, our portfolio of pasteurizers can be adapted to meet a wide range of application requirements. Customized to each customer's process needs, these hygienic pasteurization systems use tubular heat exchanger technology that supports gentle product handling, including highly viscous products and products containing particulates such as vegetable pieces or fibers.
Pasteurization units can be configured to match your required capacity and production scale, from pilot plants to industrial systems with throughputs of up to 20,000 kg/h. In addition, GEA can design and deliver complete processing lines for a broad range of liquid food applications.
User friendly switching between products
GEA pasteurizers provide user friendly design allowing easy access to all components. Inspection and maintenance can therefore be carried out with minimal downtime.
Features and benefits of GEA pasteurizers
- Tubular heat exchangers provide controlled heat treatment suitable for sensitive products
- Suitable for hygienic and aseptic processing applications
- Modular tubular heat exchanger design supports system expansion and future upgrades
- Designed for integration with automated clean-in-place (CIP) systems
- Integrated heat recovery for controlled thermal process management
- User-friendly design supports straightforward inspection and maintenance
Technologies for consistent production performance
We understand the importance of maintaining product quality, optimizing production performance, and ensuring reliable operations. That's why we continuously develop solutions designed to support your processing requirements and operational goals.
Heat recovery units are integrated as standard into our pasteurizer systems and can recover up to 60% of the heat used within the process. Where suitable, optional GEA heat pump technology can be integrated into existing plant infrastructure to provide hot water at temperatures of up to 95°C for pasteurization and cleaning-in-place (CIP) applications. Combined with the pasteurizer's integrated heat recovery unit, this solution supports reliable process heating and hot water supply for production operations.

User friendly systems backed by GEA service and support
Hygienic by design to comply with stringent regulation for food production, GEA pasteurizers are also user friendly. Easy access to all components means that regular inspection and maintenance can be carried out with minimal hands on time, and so increase equipment uptime.
Our GEA CODEX® automation platform seamlessly manages GEA pasteurizer operations and control throughout the entire process line, ensuring effortless training for personnel in operating GEA pasteurizers.
GEA also offers a range of service packages that will support you and your technology for the lifespan of the plant. Our experts can be always on hand for advice or to help troubleshoot, whether your system is configured for remote access, or we visit your site. And it’s commonly simple to adapt, expand or upgrade GEA pasteurizer plants as we launch new components and release upgrades, or when you want to expand and diversify.
Try before you buy
At our GEA test center in Ahaus you can trial your products on pilot scale GEA pasteurizers and on complete, integrated lines. Our industry, process and technology experts are there to help you define and configure the optimum equipment for your processes. We can aid with scale up so you can be confident that your GEA equipment will give you great results, from day one.


GEA Insights
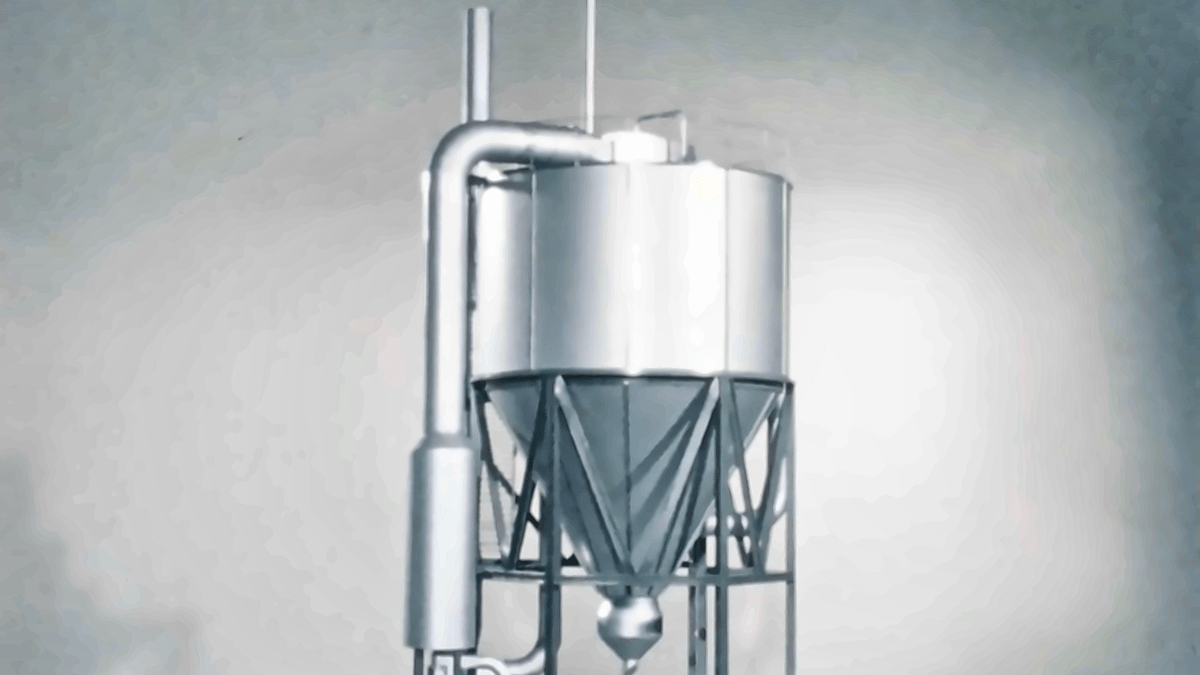
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.

Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.

How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
