

GEA OptiPartner® NiSoMate® is a stand-alone, in-line sensor-based device designed to monitor key fluid parameters continuously and in real time during the entire production cycle. Quality monitoring is based on ultrasound technology, which defines the physical characteristics of the processed fluid by analyzing variations in the speed of sound passing through the product itself.
How it works:
Its sensors and temperature probes can measure fluid properties and quality both before and after homogenization, generating reliable reference curves. The many parameters that the device monitors include particle size distribution, dilution, density, change in consistency, and temperature among others.
OptiPartner® NiSoMate® can be calibrated directly in situ and on the product(s) to set the required quality: the registered parameters are then stored in the system as reference for in-line analysis. The calibration develops a fingerprint for up to 250 configurable recipes. Then, the device measures and stores the fingerprint of each recipe in the controller, using it as the set point for product evaluation.
During production, the operator selects the recipe on the device control panel, and the device continuously compares the measured parameters to the recipe’s fingerprint. When deviations from the recipe are detected, an alarm alerts the operator, allowing them to adjust operating parameters in real time.
This minimizes product waste by ensuring consistent quality throughout production, eliminating reliance on spot sampling.
Key benefits of GEA OptiPartner® NiSoMate®:
Energy efficiency. Designed to help operators achieve the required product quality at the lowest pressure possible, optimizing energy consumption. High versatility. Tailored to customer requirements, customizable for all kinds of products, and compatible with all installations – from table-top units to industrial plants, on both new and existing machines. Safety and hygiene. CIP and SIP able, it meets even the most demanding requirements in sanitary and aseptic lines. Sensors are not in direct contact with the product for maximum safety and hygiene. Reduced waste. Automated configuration, continuous monitoring, and real-time process adjustments reduce the risk of product rework and loss. Improved plant capacity. No need to wait for laboratory analysis on product samples maximizes machine availability.
Additional benefits:
OptiPartner® and NiSoMate® are registered as trademarks in several countries worldwide.
Related Products

Homogenizers Ariete® Series
The Ariete® machines are the state-of-the-art technology for powerful reliable high-pressure homogenizers and customized solutions.

GEA Ariete® Homogenizer 5400
Ariete® Homogenizer 5400, high performance high flow-rate

GEA Ariete® Homogenizer 3160
State-of-the-art high pressure homogenizer from the Ariete® Series which is extremely versatile and highly customized for a wide range of applications: dairy, beverage, food, pharmaceutical, chemical and cosmetic industries.

Homogenizers Pilot Plant
Pilot plant homogenizers are designed for continuous operation up to 1500 bar and limited productions easy plug & play installation, simple operation and quick maintenance.
GEA Insights
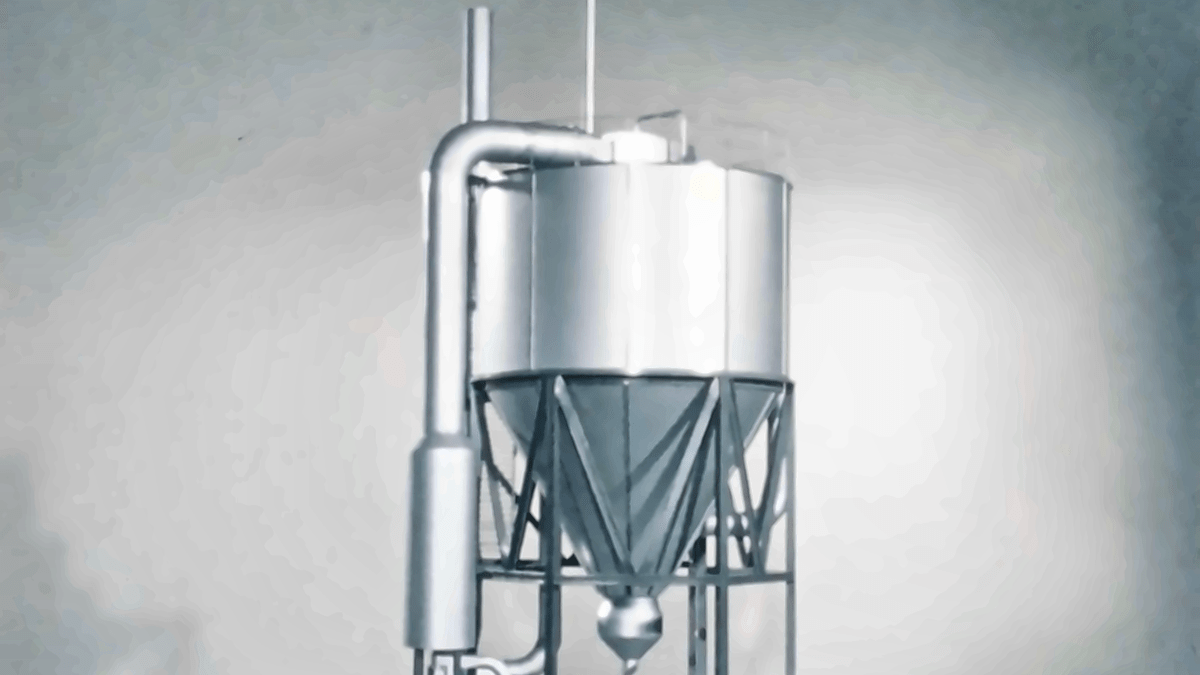
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.
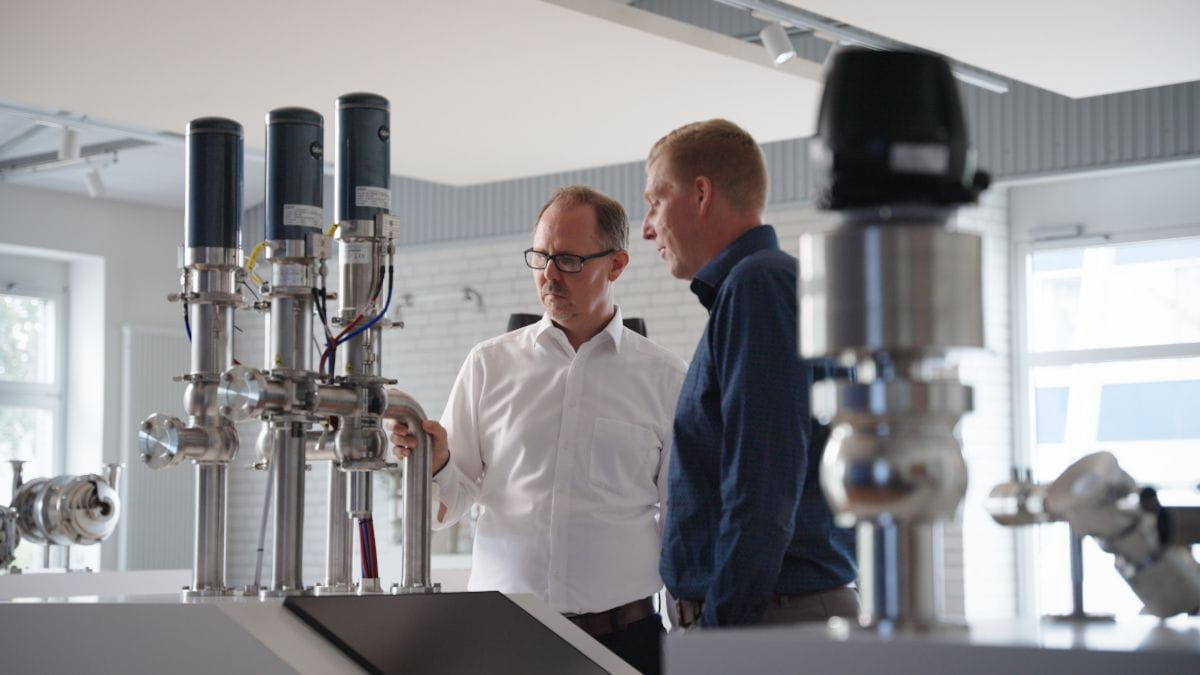
How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
