
BUCK® Sampler for Contamination-Free Sampling
Based on split valve technology, the BUCK® Sampler was specifically developed for gravity based process sampling applications in combination with commonly used product sampling equipment in processes such as granulation and drying.
The sampler offers a fully contained sampling process, even maintaining a process-related pressure resistance during all stages of docking, sampling and undocking.
Principle BUCK® Sampler
Undocked and Closed
Both the sampler and sample port are closed and sealed with a spring-loaded cover.
Docked and Closed
Connecting the sampler to the sample port forms a secure seal, without needing to stop the process.
Docked and Open
Continuing to screw the sampler to the sample port will cause the two parts to open. Both covers, the sampler and the sample port form a completely sealed unit.
Disposable Hicoflex® Sampling Technology
The Hicoflex® Sample Bag is a fully contained sampling device that enables a process sample or the bulk material in a Hicoflex® Charge Bag to be taken through an Hicoflex® Adaptor. The approx. volume of sample that can be taken is 5ml.
Downloads
Verwandte Produkte

BUCK® MC Containment Valves
BUCK® valves were the first commercially available split valves on the market. Used for the contained transfer of active powders from one vessel to another in pharmaceutical production, BUCK® technology is the result of thousands of successful applications worldwide and more than 15 years of experience.

Hicoflex® Single Use Containment System
A disposable high containment Interface for the safe & dust-free transfer of solid dosage material to fully protect your operator, your product and the environment.

Digital Canary protects your people
Based on the traditional concept of a live coal-mine canary, the 21st century equivalent from GEA is a continuous real-time monitoring system that’s been designed to detect breaches in contained pharmaceutical production lines. By providing an additional level of monitoring, the Digital Canary reduces the need for routine occupational health chec...
GEA Insights
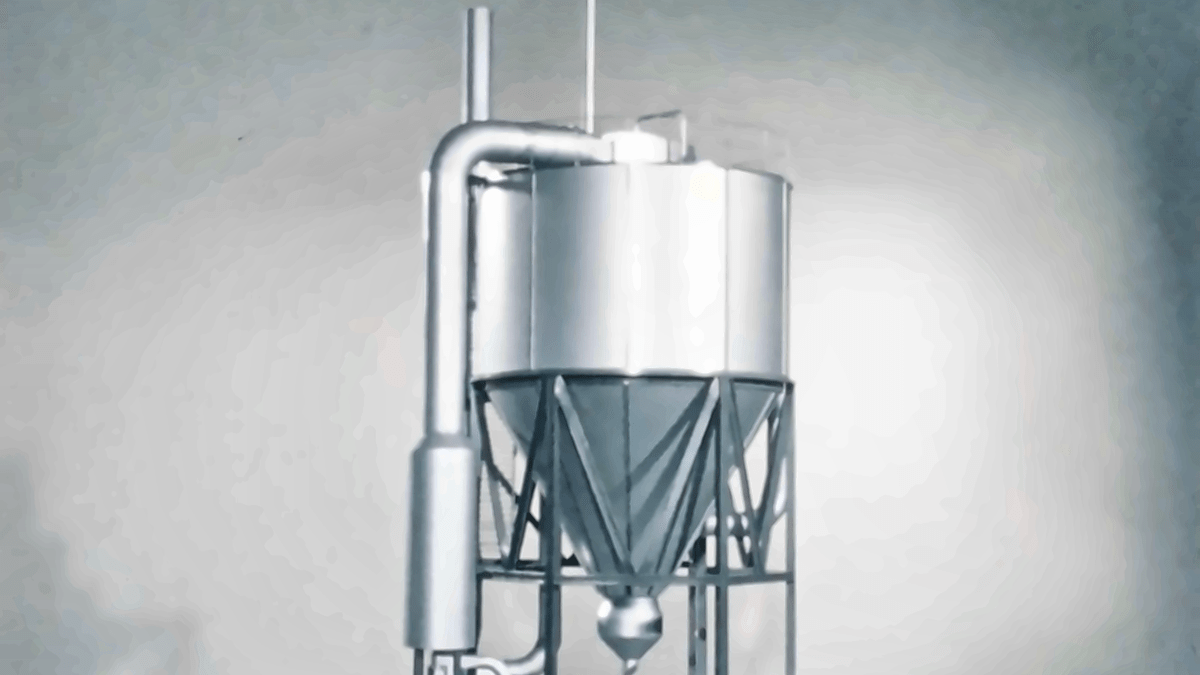
Der Durchbruch, der die Sprühtrocknung revolutionierte
Im Jahr 1976 stellten sich die Ingenieure von NIRO einer neuen Herausforderung im Wettbewerbsumfeld und überdachten die Möglichkeiten der Sprühtrocknung. Aus ihrer Idee entstand der Mehrstufentrockner MSD. Fünfzig Jahre später trägt dasselbe Grundprinzip dazu bei, Flüssigkeiten in Pulver umzuwandeln, die weltweit in unverzichtbaren Ernährungsprodukten und wichtigen Arzneimitteln zum Einsatz kommen. Der MSD wurde durch jahrzehntelanges ingenieurtechnisches Know-how, Kundenfeedback und kontinuierliche Weiterentwicklung verfeinert und steht für eine Erfolgsgeschichte der Innovation mit nachhaltiger Wirkung.

Das Ganze im Blick: Wie Anlagen dauerhaft besser laufen
Eine effiziente Maschine macht noch keine effiziente Produktion. Echte Verbesserungen beginnen oft damit, den Blick über die einzelnen Anlagenelemente hinaus zu richten und zu verstehen, wie sich Prozesse, Energiesysteme und betriebliche Entscheidungen gegenseitig beeinflussen. Ein solcher ganzheitlicher Ansatz hilft beim Identifizieren von Potenzialen, die sonst verborgen bleiben.

Wie eine neue Ventiltechnologie die Produktion von Lebensmitteln und Getränken verändert
In der Lebensmittel- und Getränkeindustrie werden Ventile traditionell mit Druckluft betrieben. Die GEA Hydract®-Antriebstechnologie betätigt Ventile dagegen mit Wasser in einem geschlossenen, digital gesteuerten Kreislauf. Das Ergebnis: Ventile lassen sich präzise in jeder gewünschten Position halten und in fein abgestuften Schritten steuern. Dadurch sinken der Energieverbrauch und gleichzeitig steigt die Prozesskontrolle erheblich.
